HVOF Thermal Spraying System — Oil-Fuel Supersonic Flame
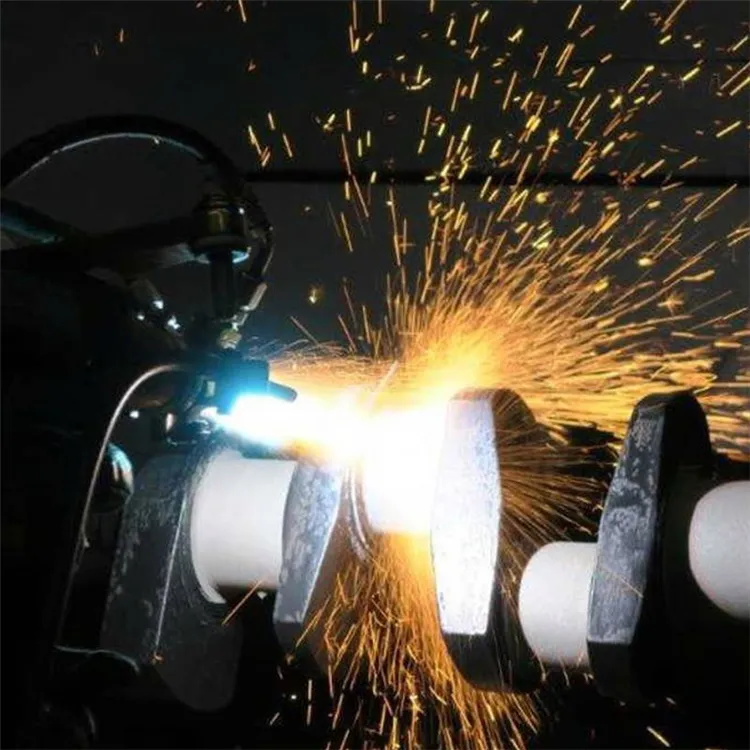
The system atomises kerosene with oxygen; the mixture enters the combustion chamber, is ignited, and forms a high-pressure supersonic flame through a Laval nozzle. Powder is injected into the flame stream from the low-pressure zone, heated and accelerated onto the workpiece to form dense, high-quality carbide coatings.
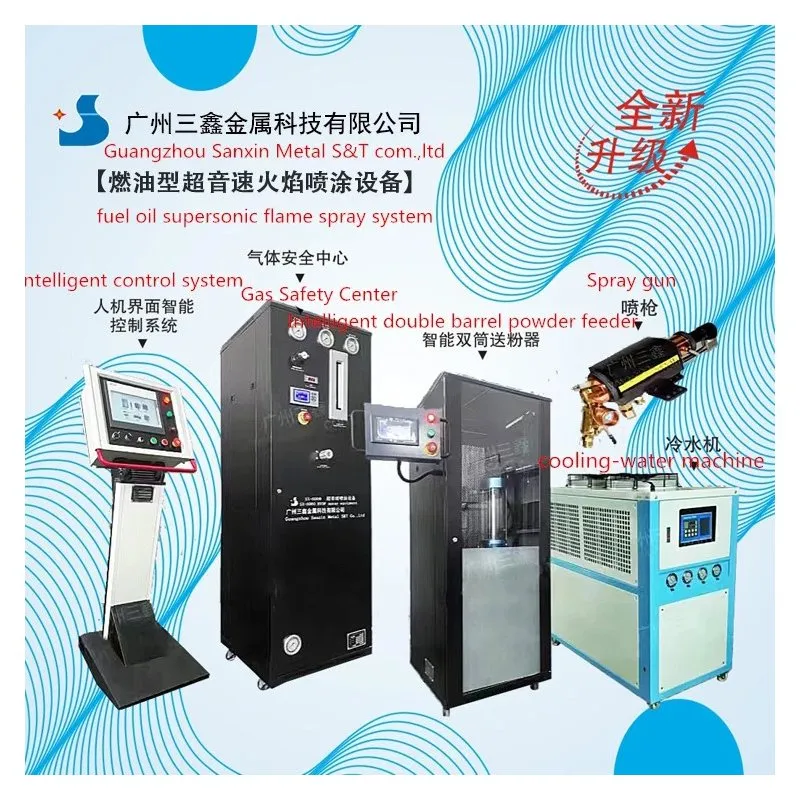
System configuration
- HVOF spray gun (oil fuel)
- Intelligent double-barrel powder feeder
- Human-machine interface control system with PLC
- Gas safety center
- Industrial water chiller
Technical parameters
- Flame temperature: 2,700 °C
- Coating bond strength: >70 MPa
- Oxygen pressure: 1.1 MPa; propane 0.65 MPa; air 0.8 MPa
- Powder feeding gas: nitrogen at 1.2 MPa
- Weight: approx. 700 kg (system); footprint approx. 2.8 m³
Why HVOF
- Extremely dense coatings with low oxide content
- Compressive residual stress allows thick carbide builds
- Environmentally friendly alternative to hard chrome plating