Application fields:
Industrial plant structures, pipe racks and platforms, steel frames in chemical plants, coastal and offshore structures, water treatment works steelwork, and refurbishment of rusted fabricated steel.
Technical principles and processes:
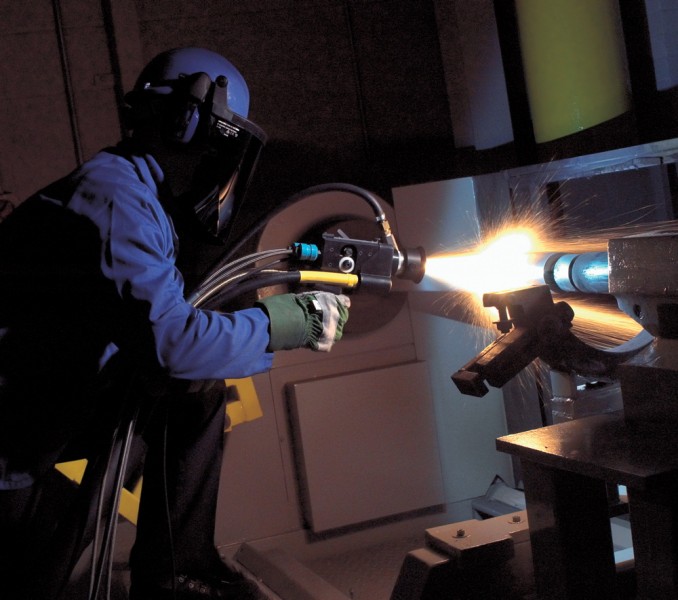
Existing rust and old coating are removed by abrasive blasting to the specified surface preparation grade. A zinc or zinc-aluminum coating is applied by arc spray, followed by a sealer and a compatible topcoat system. Adhesion and thickness are inspected before the topcoat is applied.
Coating performance:
- Combined system life substantially longer than paint alone
- Sacrificial protection tolerates local mechanical damage
- Coating thickness 100-200 microns before topcoat
- Suitable for coastal, humid and mildly chemical atmospheres
- Inspection record covering preparation, thickness and adhesion
钢结构防腐表面处理:喷砂除锈后电弧喷涂锌或锌铝层,再配套封闭漆与面漆,防腐年限显著优于单纯油漆体系,适用于沿海、潮湿与化工环境。
System specification
| Coating | Thickness | Service environment | Expected life |
|---|---|---|---|
| Zinc (Zn 99.9%) | 80-150 µm | Industrial and rural atmosphere | 15-25 years |
| Zinc-aluminium 85/15 | 100-200 µm | Coastal, marine, humid | 20-30 years |
| Aluminium (Al 99.5%) | 100-200 µm | High temperature, sulphur-bearing atmosphere | 20-30 years |
| Zn-Al + epoxy seal | 150-250 µm total | Immersion, splash zone, chemical plant | 25-40 years |
Why metallising beats paint in severe environments
A paint system is a barrier: once it is breached, corrosion runs underneath and lifts the coating. A thermally sprayed zinc or aluminium layer works differently - it is sacrificial, so a scratch or a weld seam is protected by the surrounding metal rather than becoming the starting point of failure. That is why ISO 2063 metallising is specified for offshore structures, lock gates, bridges and chemical plant steelwork where repainting access is expensive.
Surface preparation is the whole job
- Grit blast to Sa 3 (ISO 8501-1) with angular grit, profile 75-125 µm.
- Spray within four hours of blasting; if the steel flashes rust, blast again.
- Edge preparation: radius or chamfer sharp edges before blasting, or the coating will be thin there.
- Seal with a low-viscosity epoxy to fill porosity, then apply the specified topcoat.
Frequently asked questions
Can metallising be applied over existing paint?
No. The coating needs a clean, blasted steel surface to bond. Existing paint must be removed, and any corroded areas cut out or repaired first.
How does the cost compare with a paint system?
Material cost is higher, but in C4-C5 environments the life-cycle cost is usually lower because the interval between maintenance campaigns is measured in decades rather than years.
Is it suitable for immersion service?
Yes, with a sealed system - Zn-Al plus epoxy seal is standard for splash zones and tank exteriors in seawater.
Further reading: What drives coating cost per part.