Application fields:
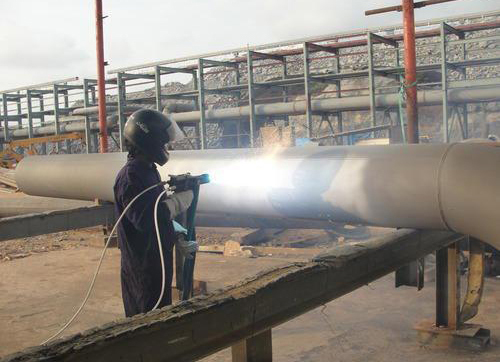
Process and utility pipelines, penstocks and large diameter pipe, tank exteriors and internals, crane rails and rails in service, and steel structures that cannot be dismantled for coating.
Technical principles and processes:
The area is isolated, cleaned and abrasive blasted in a contained zone. Arc spray or flame spray equipment is then set up at the worksite and the coating is applied to the specified thickness, with the same preparation and inspection standard used in the workshop. Topcoats are applied where required.
Coating performance:
- Coating applied in place, no dismantling or transport cost
- Arc spray zinc-aluminum or zinc coating for corrosion protection
- Carbide coatings available for wear areas such as pipe bends
- Thickness verified on site with a magnetic gauge
- Work scheduled around plant shutdowns wherever possible
管道现场热喷涂:针对无法拆运的大型管道与钢结构,派工上门做表面处理与喷涂,现场恢复防腐或耐磨性能,减少停机与运输成本。
Field coating specification
| Item | Specification |
|---|---|
| Process | Portable arc spray (twin wire), 300 A class |
| Coating | Zn, Zn-Al 85/15 or Al, 100-250 µm |
| Surface prep | Sa 2.5-3 by vacuum-assisted blasting or bristle blasting |
| Access | Rotating pipe or orbital gun carriage for 6-48 inch lines |
| Seal | Epoxy or polyurethane, applied within the same shift |
| Standard | ISO 2063, NACE SP0188 for holiday detection |
When on-site is the right call
A pipeline that cannot be cut, a tank that cannot be drained, a crane rail in a live plant - these are the cases where dismantling costs more than the coating itself. Portable arc spray operates from a 30 kW generator, so it can be set up next to the structure with local extraction and no fixed booth.
The limitation is access, not the process. Coating quality on site depends almost entirely on how well the surface can be blasted; if the geometry prevents a proper Sa 2.5 profile, the coating will not reach its design life.
Frequently asked questions
How much area can be coated per day on site?
Typically 15-40 m² per day for a two-person crew, depending on access, scaffolding and the number of coating layers.
Can it be done on a live pipeline?
Only where the surface temperature is within limits and the plant permits hot work. Cold processes are used near live equipment; the operating authority's permit governs.
How is quality verified in the field?
Thickness by magnetic gauge at a defined grid, adhesion by pull-off test on a witness area, and holiday detection on immersion-bound sections.
Further reading: What drives coating cost per part.