Application fields:
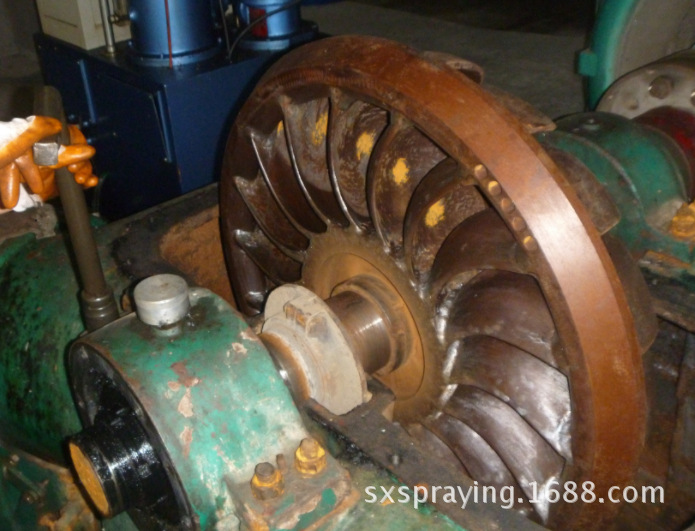
Slurry pumps in mining and mineral processing, dredging and sand handling pumps, seawater and desalination pumps, chemical process pumps, and circulating pumps handling solids-laden media.
Technical principles and processes:
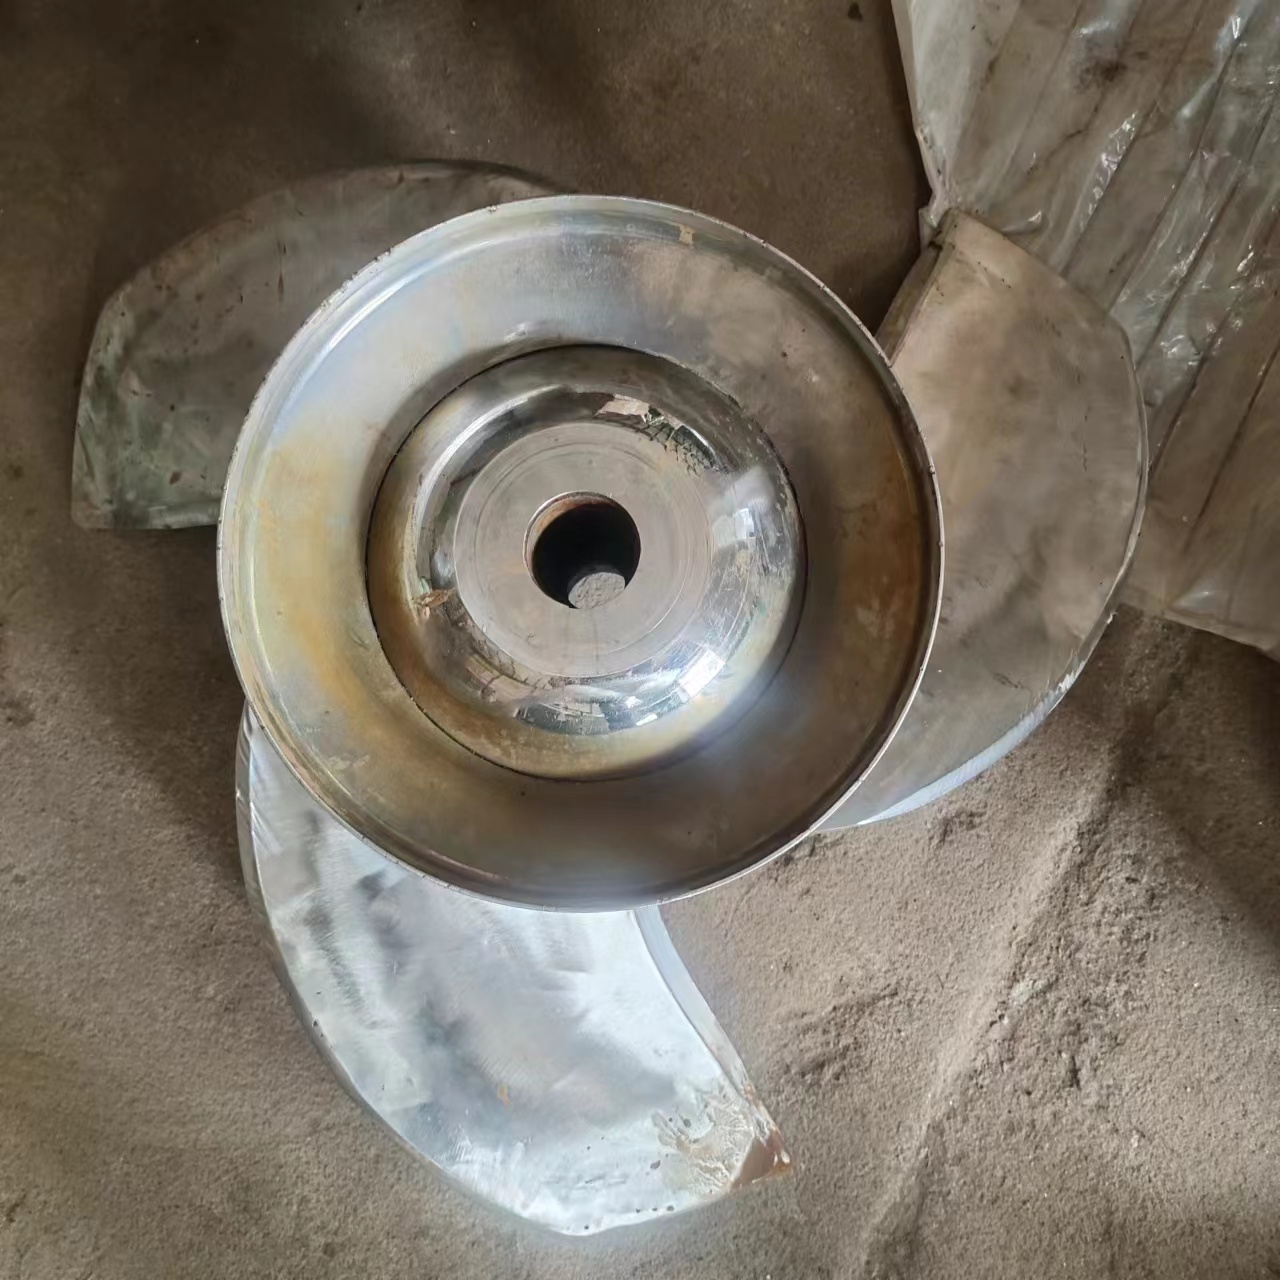
The impeller is stripped of any previous coating, inspected for cracks, and grit blasted. Worn areas are rebuilt to profile where required, then a HVOF tungsten carbide coating is applied to the vane faces, leading edges and hub. The impeller is dynamically checked and finish ground so the flow passages stay within tolerance.
Coating performance:
- Micro-hardness 1100-1400 HV for erosion resistance
- Coating thickness 0.20-0.50 mm in high-wear zones
- Erosion rate reduced by 60-80% versus uncoated cast iron
- Pump efficiency and head recovered on worn impellers
- Balanced, ground finish so vibration stays within limits
水泵叶轮碳化钨涂层加工:针对含砂、矿浆、海水等磨蚀工况,对叶片流道与轮缘做超音速火焰喷涂碳化钨,既可修复磨损叶轮,也可用于新件预保护。
Coating specification
| Parameter | Typical value |
|---|---|
| Coating | WC-Co or WC-CoCr, HVOF |
| Thickness | 0.15-0.40 mm on vane faces and shrouds |
| Microhardness | 1,050-1,300 HV0.3 |
| Porosity | Below 1% |
| Bond strength | 70 MPa minimum |
| Surface finish | Ra 0.8-1.6 (hydraulic efficiency vs. wear trade-off) |
Why slurry pumps fail at the vane, not the hub
In a slurry pump, the particle-laden flow accelerates through the impeller passage and impacts the trailing face of each vane at a shallow angle - the classic erosion regime. Material loss there opens the clearance, recirculation increases, and efficiency falls off a cliff long before the impeller looks damaged. Coating the vane faces and the wear ring area restores the geometry that efficiency depends on.
Preparation matters more than on a new part
Worn impellers arrive with a profile that is no longer the design profile. Coating a worn vane just preserves the wrong shape. We build up the eroded area first, grind back to the original section, then apply the carbide layer - which is slower but is the only way to recover both efficiency and wear life.
Frequently asked questions
Can the coating be applied to a rubber-lined pump?
No. HVOF needs a metallic substrate. Rubber-lined pumps are usually converted to coated metal impellers, or kept as they are.
Will the coating chip on large particles?
WC-CoCr at 0.2-0.3 mm handles most slurries. Where rocks or tramp metal are present, a tougher WC-12Co or a duplex build-up is used instead.
How long does recoating take?
Seven to ten working days including build-up, spraying, grinding and balancing - usually faster than a new impeller lead time.
Further reading: WC-Co vs Cr3C2-NiCr.