Application fields:
Chemical and pharmaceutical mixing tanks, mineral and ceramic slurry mixers, food processing agitators, pigment and coating production, and any mixer blade that runs continuously in an abrasive or mildly corrosive medium.
Technical principles and processes:
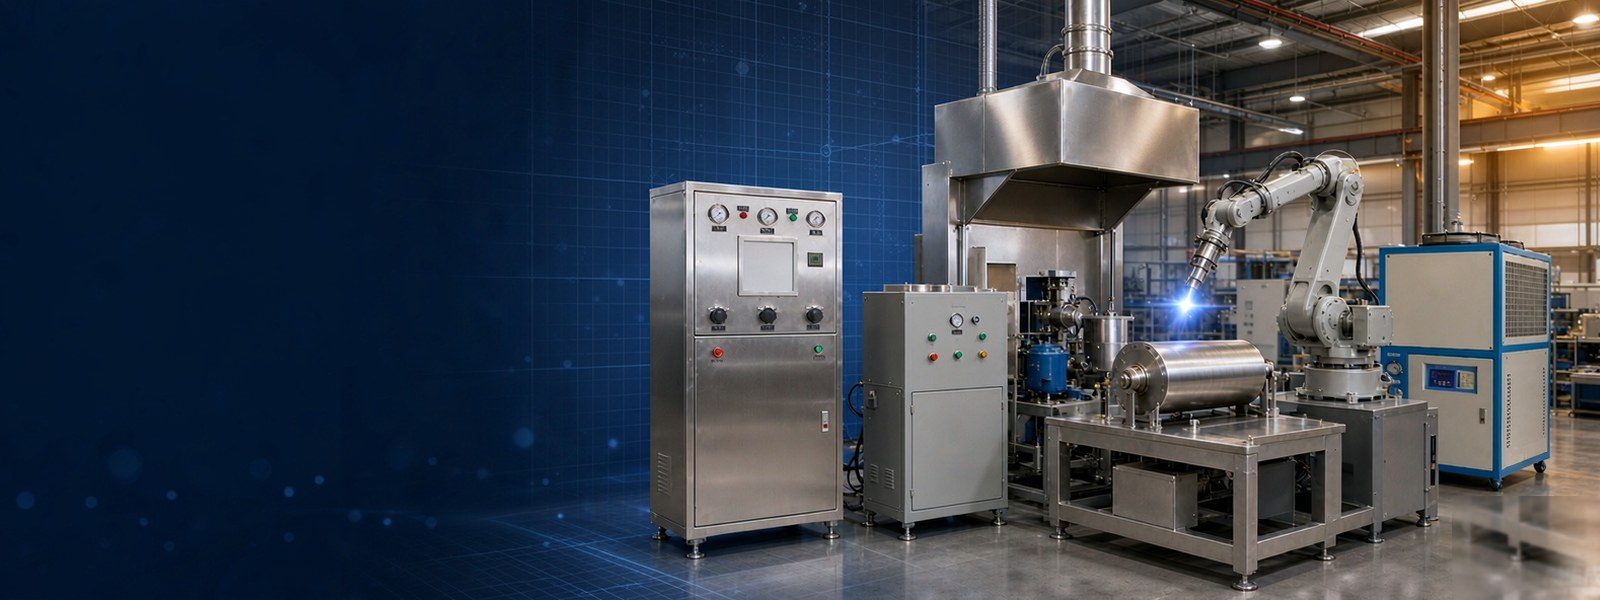
The blade is dismantled, cleaned and grit blasted to a controlled roughness to key the surface. A tungsten carbide-cobalt (WC-Co) or WC-CrC-Ni powder is then sprayed by high velocity oxy-fuel (HVOF), producing a low-porosity, tightly bonded coating. The blade is finish ground where dimensional accuracy matters, and coating thickness is checked across the working face.
Coating performance:
- Micro-hardness 1200-1400 HV, well above hardened steel
- Typical coating thickness 0.15-0.40 mm, adjustable to wear rate
- Bond strength above 70 MPa, no flaking under impact loading
- Service life extended 3-8 times compared with uncoated blades
- Surface roughness and thickness recorded on a coating report
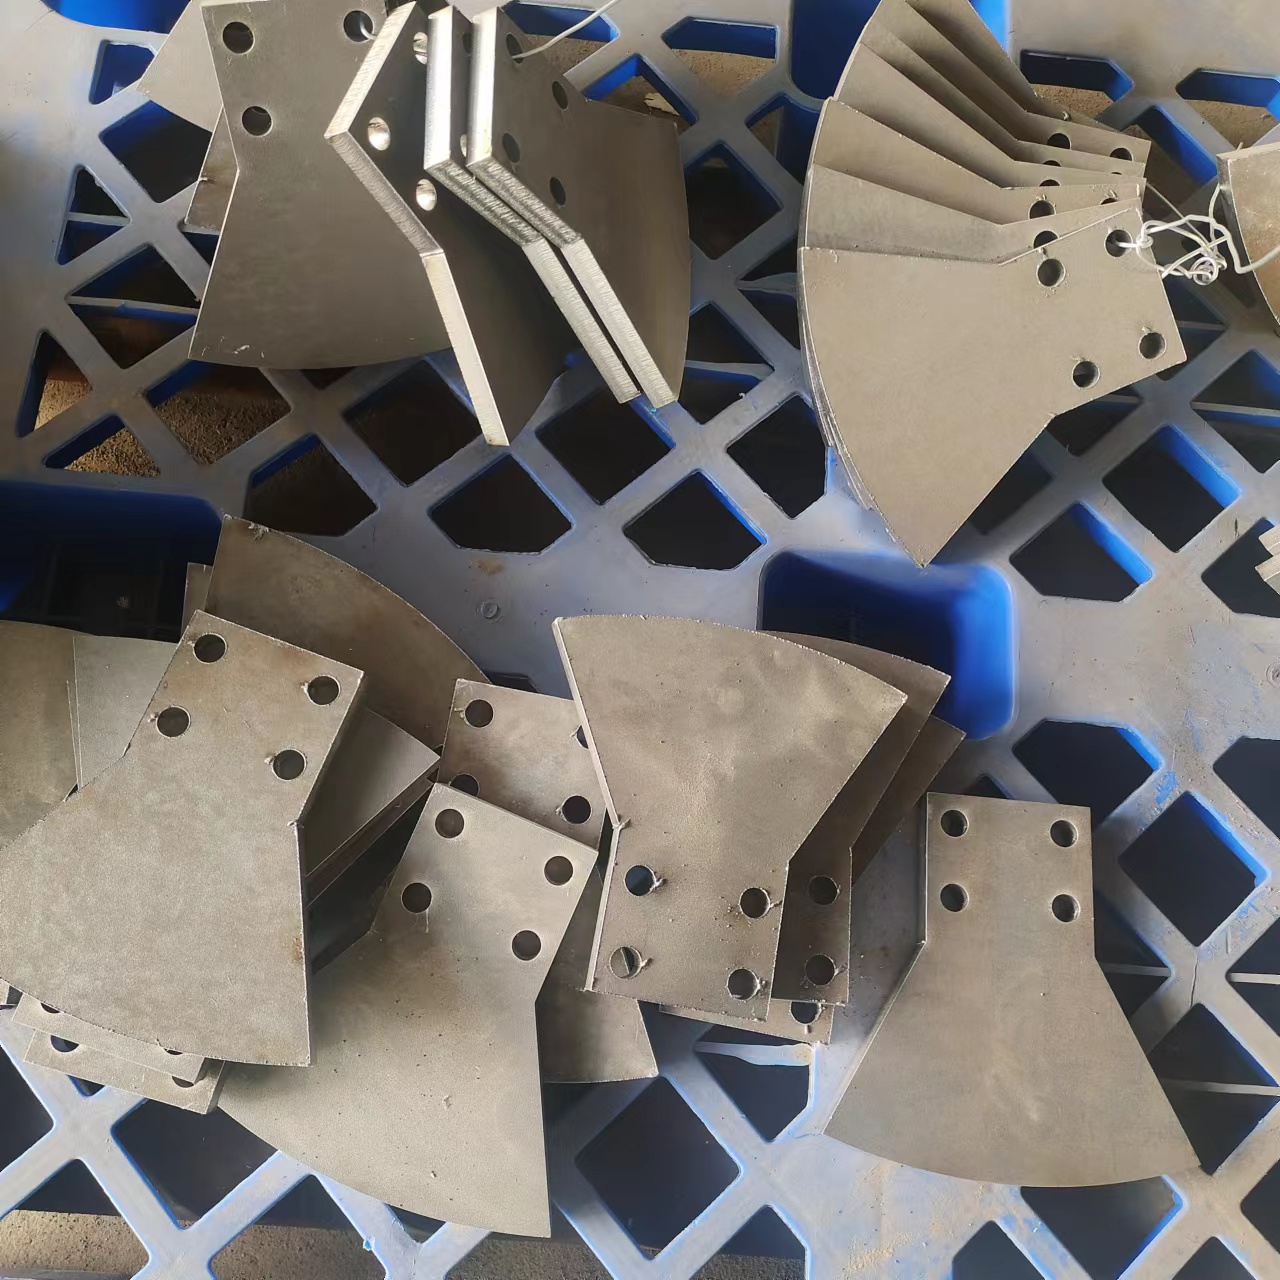
搅拌机叶片碳化钨涂层加工:针对磨蚀性浆料、粉体与腐蚀介质工况,对叶片工作面做超音速火焰喷涂碳化钨,显著延长使用寿命,减少停机换件。
Coating options by duty
| Medium | Coating | Thickness |
|---|---|---|
| Mineral or ceramic slurry | WC-Co, HVOF | 0.20-0.35 mm |
| Chemical with acid/alkali | WC-CoCr, sealed | 0.20-0.35 mm |
| Food or pharma, metal-sensitive | Al2O3 or Cr2O3 | 0.20-0.30 mm |
| High-solids pigment or coating | Al2O3-TiO2 | 0.25-0.40 mm |
Where blades wear
The tip and the leading edge see the highest relative velocity, so they erode first - often two to three times faster than the blade face. Coating a blade at uniform thickness is a compromise; we thicken the tip zone and taper the layer towards the hub, which also keeps the blade balanced.
Food and pharmaceutical duty
Where the mixer contacts product, alumina or chromia is used instead of carbide because it contains no cobalt. Coatings are sealed, ground smooth and inspected for exposed bond coat; material certificates are supplied with the order.
Frequently asked questions
Can a coated blade still be welded or modified?
The coating must be stripped locally before welding, then reapplied. Welding through a carbide layer produces porosity and cracks that spread into the coating.
How do I know when to recoat?
When the tip radius has doubled or the coating is visibly worn through to a different colour. Measuring the tip profile at each shutdown is the simplest tracking method.
Does coating change mixing performance?
Only if the layer is thick enough to alter the profile. At 0.3 mm on a 300 mm blade the hydraulic effect is negligible.
Further reading: WC-Co vs Cr3C2-NiCr.