Application fields:
Chemical and pharmaceutical mixing tanks, mineral and ceramic slurry mixers, food processing agitators, pigment and coating production, and any mixer blade that runs continuously in an abrasive or mildly corrosive medium.
Technical principles and processes:
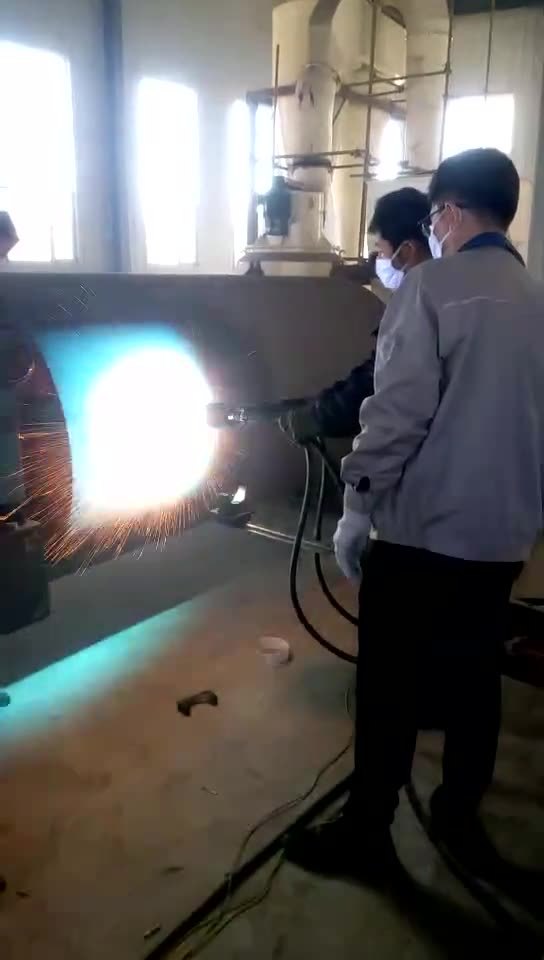
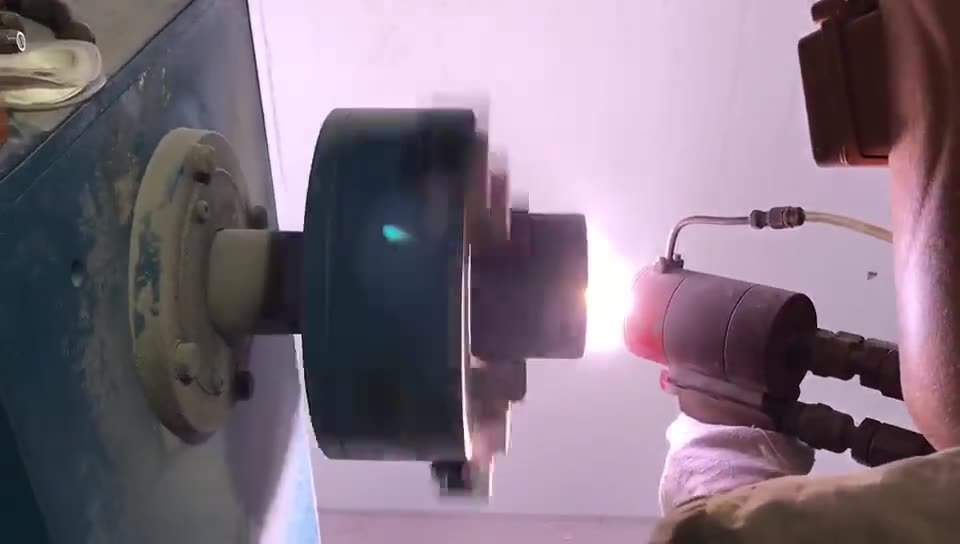
The blade is dismantled, cleaned and grit blasted to a controlled roughness to key the surface. A tungsten carbide-cobalt (WC-Co) or WC-CrC-Ni powder is then sprayed by high velocity oxy-fuel (HVOF), producing a low-porosity, tightly bonded coating. The blade is finish ground where dimensional accuracy matters, and coating thickness is checked across the working face.
Coating performance:
- Micro-hardness 1200-1400 HV, well above hardened steel
- Typical coating thickness 0.15-0.40 mm, adjustable to wear rate
- Bond strength above 70 MPa, no flaking under impact loading
- Service life extended 3-8 times compared with uncoated blades
- Surface roughness and thickness recorded on a coating report
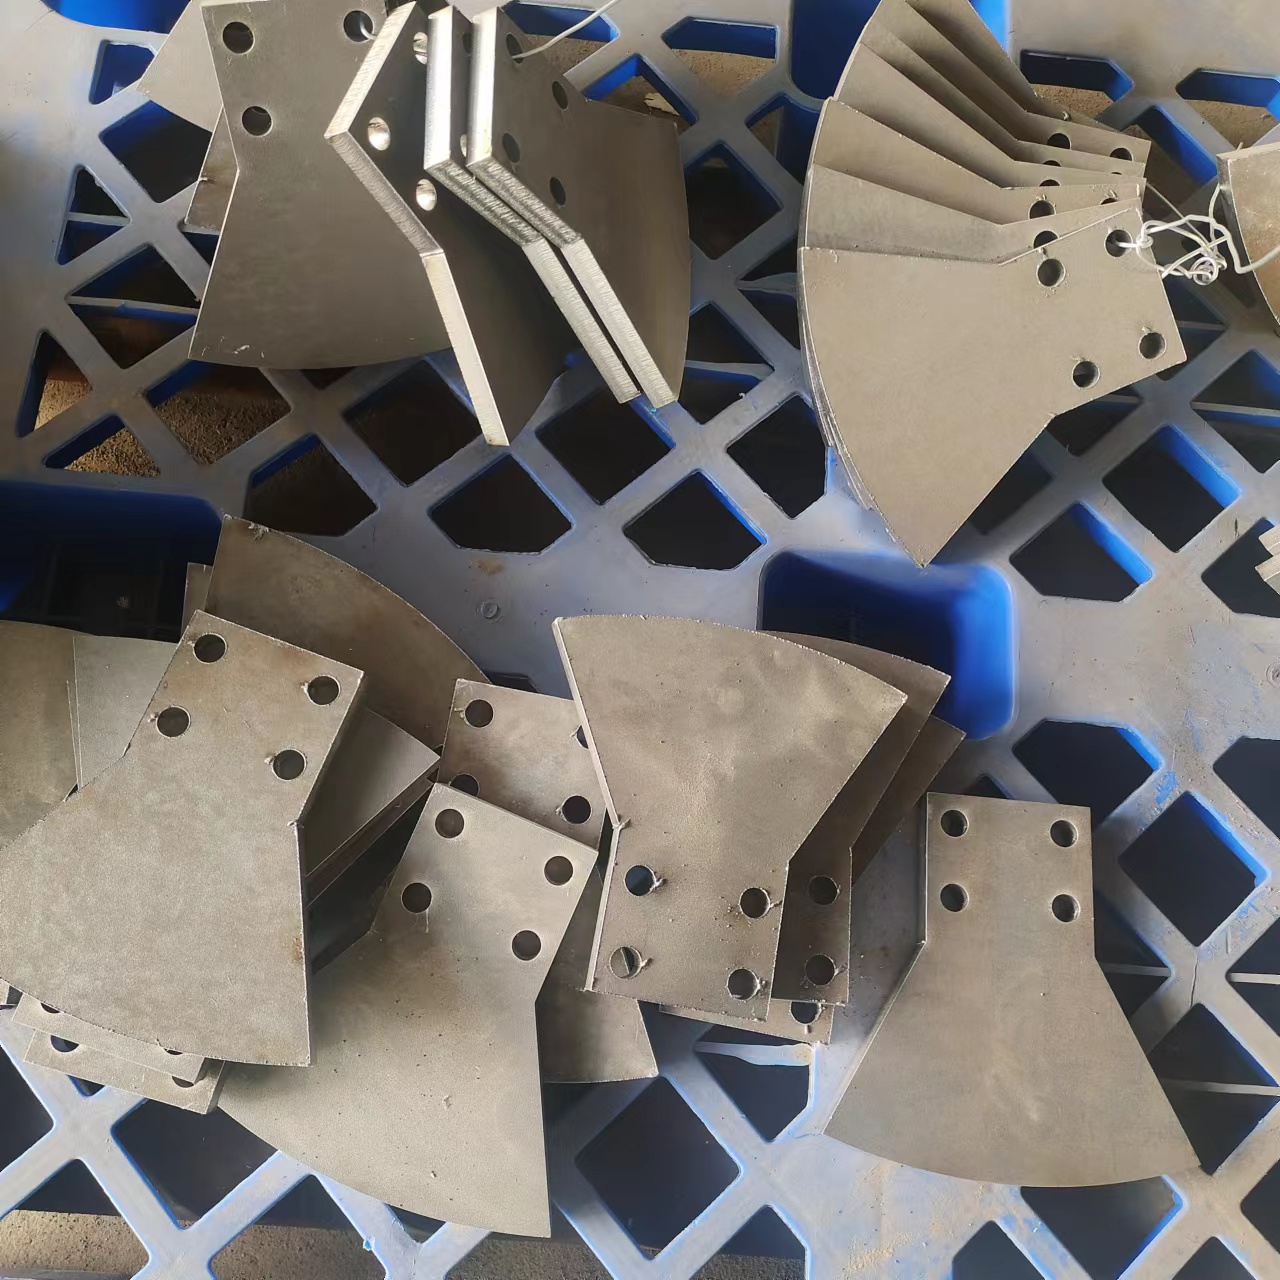
搅拌机叶片碳化钨涂层加工:针对磨蚀性浆料、粉体与腐蚀介质工况,对叶片工作面做超音速火焰喷涂碳化钨,显著延长使用寿命,减少停机换件。
Coating options by duty
| Medium | Coating | Thickness |
|---|---|---|
| Mineral or ceramic slurry | WC-Co, HVOF | 0.20-0.35 mm |
| Chemical with acid/alkali | WC-CoCr, sealed | 0.20-0.35 mm |
| Food or pharma, metal-sensitive | Al2O3 or Cr2O3 | 0.20-0.30 mm |
| High-solids pigment or coating | Al2O3-TiO2 | 0.25-0.40 mm |
Where blades wear
The tip and the leading edge see the highest relative velocity, so they erode first - often two to three times faster than the blade face. Coating a blade at uniform thickness is a compromise; we thicken the tip zone and taper the layer towards the hub, which also keeps the blade balanced.
Food and pharmaceutical duty
Where the mixer contacts product, alumina or chromia is used instead of carbide because it contains no cobalt. Coatings are sealed, ground smooth and inspected for exposed bond coat; material certificates are supplied with the order.
What drives the cost of coating a blade set
Four things decide the price, in this order: the coated area, how much build-up is needed to restore the worn profile, the masking complexity around the hub and any welded seams, and the finishing tolerance. A blade set that only needs a wear layer is a straightforward job; one that has lost its profile needs welding, straightening and re-machining before any coating happens - and that work, not the carbide, is usually the larger part of the quote.
How the coating is verified
Thickness is measured at several points on the face and at the tip, microhardness is checked on a coupon sprayed in the same run, and the blade is inspected for exposed bond coat and edge chipping. The report records thickness map, hardness, surface finish and the parameter set used, so the next recoating of the same blade starts from a known baseline rather than from scratch.
When coating is not the right answer
If the blade is cracked at the weld, bent beyond straightening, or worn so thin that the remaining section cannot carry the load, a coating will not fix it - replacement or re-fabrication comes first. The same applies where the medium contains large tramp metal: impact damage will spall any sprayed layer, and a different design (heavier section, rubber lining, or a screened feed) is the real solution.
Frequently asked questions
Can a coated blade still be welded or modified?
The coating must be stripped locally before welding, then reapplied. Welding through a carbide layer produces porosity and cracks that spread into the coating.
How do I know when to recoat?
When the tip radius has doubled or the coating is visibly worn through to a different colour. Measuring the tip profile at each shutdown is the simplest tracking method.
Does coating change mixing performance?
Only if the layer is thick enough to alter the profile. At 0.3 mm on a 300 mm blade the hydraulic effect is negligible.
Further reading: WC-Co vs Cr3C2-NiCr.