Ceramic Coating for Printing Machine Rollers
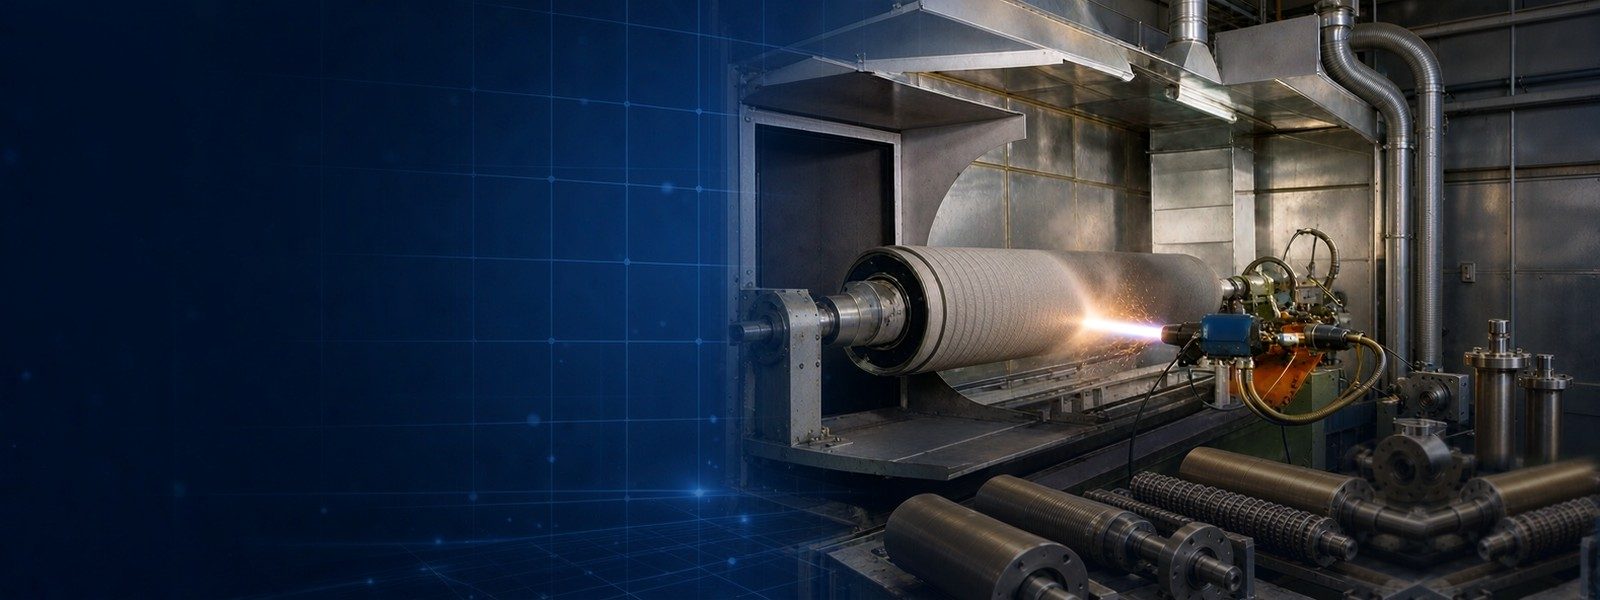
Printing, packaging and film-treating machines rely on rubber rollers, corona rollers and guide rollers that suffer constant abrasion, high surface temperature and, in corona stations, high electric field strength. A plasma or HVOF sprayed ceramic layer turns a standard metal or rubber roller into a hard, insulating, heat-resistant working surface.
Two Process Options
- Plasma spraying of alumina-based ceramics: the preferred solution where electrical insulation is the primary requirement, for corona rollers and static-eliminating rollers.
- HVOF spraying of dense carbide or ceramic composites: the preferred solution where combined wear, heat and corrosion resistance dominate, for nip rollers and high-speed guide rollers.
What the Coating Delivers
- Electrical insulation that survives continuous corona discharge and ozone exposure.
- Surface hardness far beyond rubber or polymer lining, so the surface does not groove or pick up ink and adhesive residue.
- High-temperature oxidation resistance for hot-nip and drying-section positions.
- A ground and polished finish with Ra 0.20 or better for even film contact.
Roller Refurbishment Service
Used and worn rollers are accepted. Old coating or degraded rubber is stripped, the journal is inspected, a new ceramic layer is applied, and the roller is precision ground and polished back to the original dimension and run-out tolerance.
Roller coating options
| Coating | Process | Thickness | Typical duty |
|---|---|---|---|
| Al2O3 ceramic | Plasma | 0.30-0.60 mm | Corona and treater rollers, electrical insulation |
| Cr2O3 ceramic | Plasma | 0.20-0.40 mm | Print and metering rollers, low friction, fine finish |
| WC-CoCr | HVOF | 0.10-0.25 mm | Web handling rolls, wear against film and foil |
| Al2O3 + sealer | Plasma | 0.50-1.00 mm | High-voltage insulation with ozone exposure |
Grinding and balance
Rollers are judged on runout and finish as much as on hardness. Coated rollers are cylindrically ground with diamond tooling, then polished to the specified Ra, and dynamically balanced to ISO 1940 G2.5 where speed demands it. A roller that measures correct thickness but runs out by 0.05 mm will mark the web, so balance and concentricity are checked on every roll.
Common failure modes and prevention
| Failure | Cause | Prevention |
|---|---|---|
| Coating spalls in bands | Oil or grit trapped under the layer | Degas castings, clean grit, spray immediately after blasting |
| Edge chipping | Sharp shoulder, thin coverage at the end | Radius the edge, over-travel the gun, map thickness at both ends |
| Breakdown under voltage | Connected porosity, no sealer | Seal after grinding, hipot test every roller |
Frequently asked questions
Do you coat the roller journals as well?
No. Journals, bearing seats and drive features are masked. Only the functional face is coated, and masking is included in the quoted price.
Can you match an existing coating thickness from another supplier?
Yes. We measure the existing layer and reproduce it, or recommend a change if the measured build is outside a sensible design window.
How is the roller packed for shipping?
Coated faces are wrapped in acid-free paper, the roll is supported on its journals in a wooden crate, and lifting points are marked. Export packing and documentation are arranged on request.
Further reading: why ceramic coatings fail on rollers.