Special Anti‑Wear & Anti‑Corrosion Coating Solutions
for Battery Cathode & Anode Material Grinding Equipment
Application Fields:
High‑purity powder grinding & milling equipment for lithium‑ion battery cathode materials (such as NCM, LFP) and anode materials (graphite, silicon‑carbon).
✅ Core Advantages
Ultra‑High Hardness & Wear Resistance
Adopting nano‑ceramic composite technology with alumina, silicon carbide, boron nitride particles. Surface hardness reaches HRC 65–75, significantly extending equipment service life.
Zero Metal Contamination Design
Coating contains no magnetic impurities such as Fe, Ni, Cr. Ensures high purity of battery materials and avoids negative impacts on cell performance.
Excellent Corrosion Resistance
Resists electrolyte residues, acid/alkali cleaning agents and humid environments, suitable for harsh working conditions.
Strong Adhesion & Thermal Stability
Applied by plasma spraying or HVOF process. Bonding strength >70 MPa, operating temperature range -50℃ ~ 600℃.
Customized Services
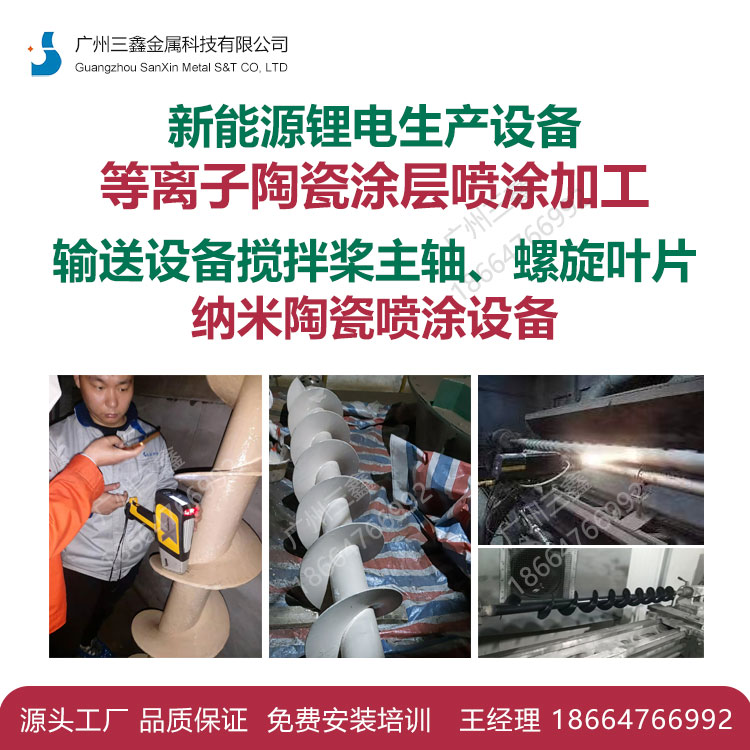
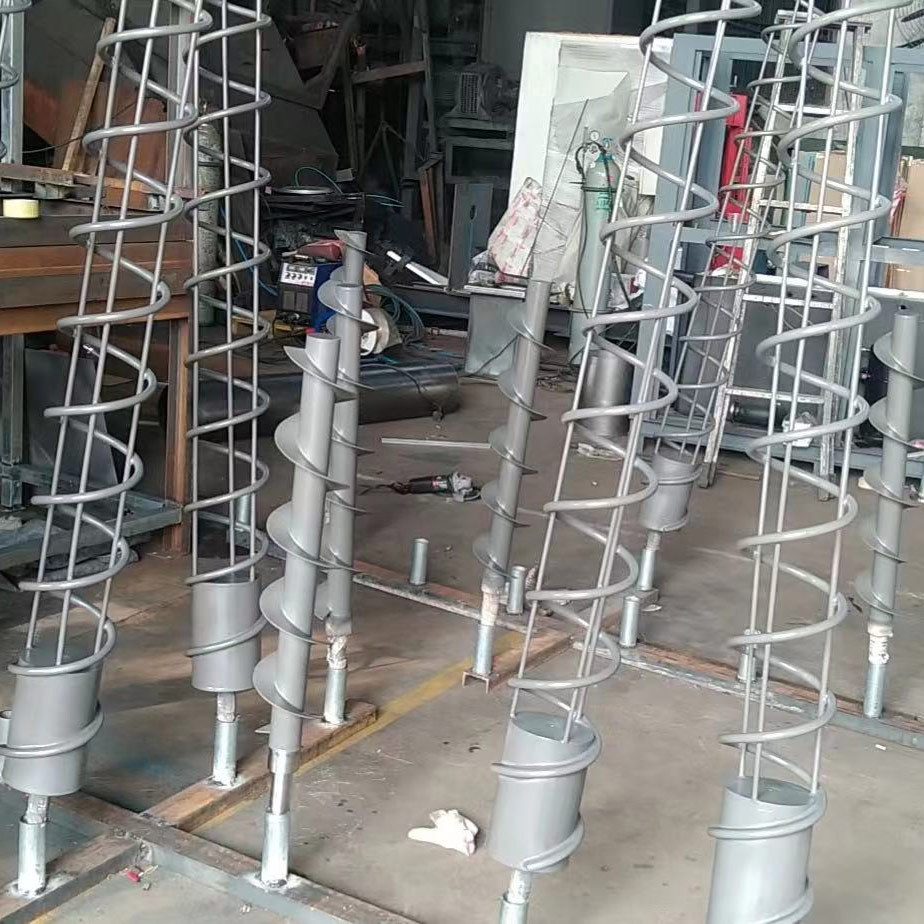
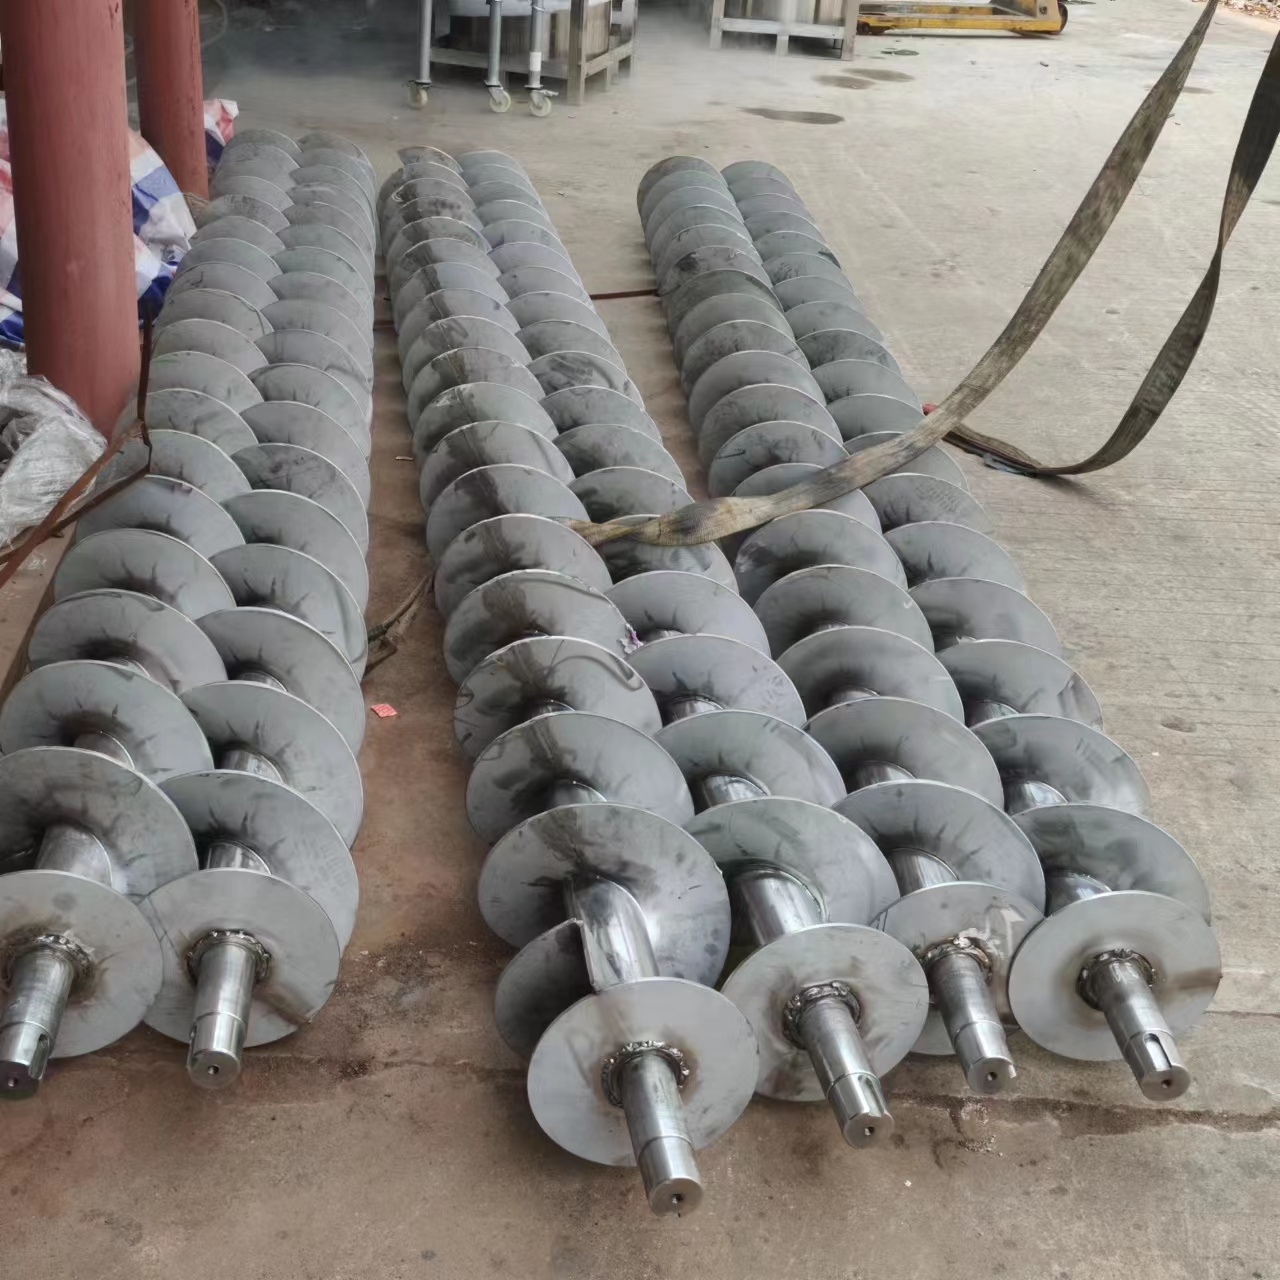
Provide partial or full coating solutions according to grinder models (jet mill, ball mill, mechanical impact mill) and worn parts (liners, classifiers, nozzles, etc.).
Application Effects
Equipment maintenance cycle extended by 2–3 times
Downtime and replacement costs reduced by over 30%
Ensures consistency and batch stability of battery materials
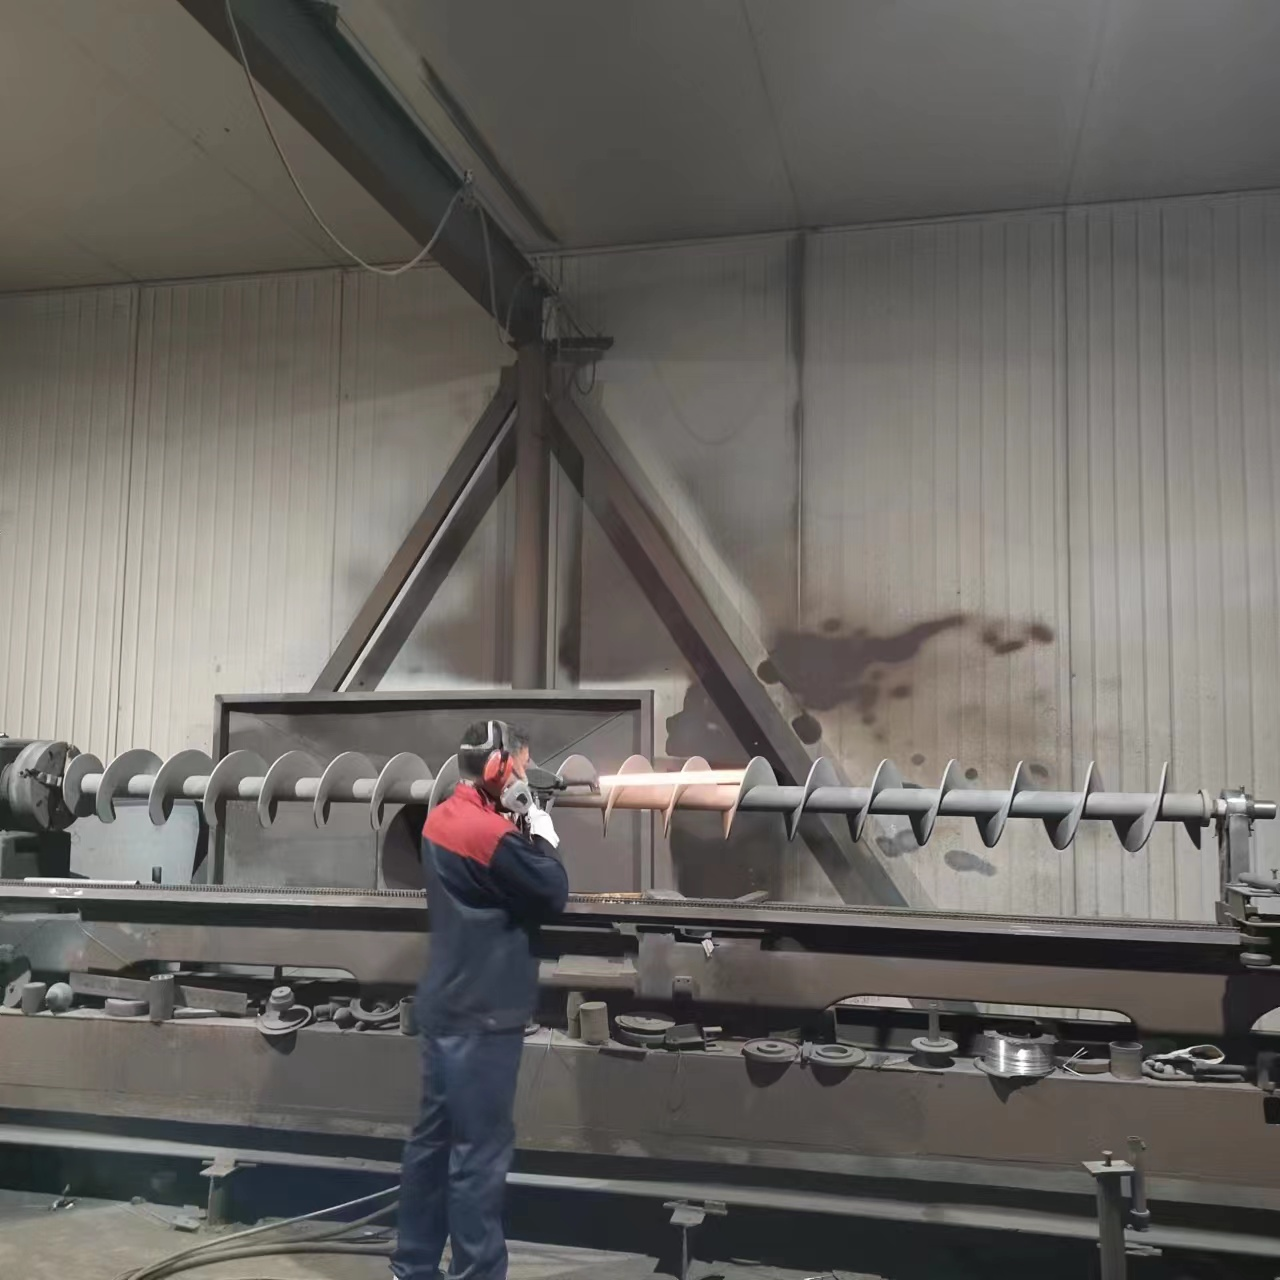
Coating specification
| Parameter | Typical value |
|---|---|
| Coating | Al2O3-TiO2 composite or alumina-zirconia blend |
| Thickness | 0.30-1.00 mm on liners and hammers |
| Microhardness | 850-1,100 HV0.3 |
| Bond strength | 40-60 MPa with NiAl bond coat |
| Porosity | 2-5%, sealed on product-contact surfaces |
| Contamination | Cobalt-free and nickel-free in the product zone |
Why a composite rather than pure alumina
Pure alumina is hard but brittle; under the impact of a crusher hammer it chips at the edges. Adding titania to the ceramic raises toughness at a small cost in hardness, which is the right trade for a part that sees both abrasion and impact. On the liner plates, where impact is lower and sliding wear dominates, a higher-alumina blend is used instead.
Sealing and cleaning between campaigns
Because the same equipment may switch between cathode and anode material, coating porosity has to be sealed so material from one campaign does not lodge in the surface and contaminate the next. Sealed coatings can be washed down between campaigns; unsealed ones cannot.
Which parts are coated
On a jet mill, ball mill or mechanical impact mill the wear is concentrated in a small number of parts: liner plates, the classifying wheel, the grinding nozzles or hammer tips, the feed injector and the outlet duct. Coating all of them is not always necessary - the practical approach is to coat the liner and the classifier first, measure the service interval, then extend the programme to the nozzles and duct where the erosion pattern justifies it.
Proving there is no contamination
For battery material customers the acceptance question is not only "how hard is the coating" but "what does it put into the powder". The coating is specified cobalt-free and nickel-free in the product zone, and the verification is done by analysing the powder before and after a run rather than by trusting a certificate: metallic impurity content and magnetic particle count are compared against the incoming material. That data, not the hardness number, is what closes the qualification with a cathode or anode material customer.
Thickness against the mill's clearances
A jet mill runs on precise internal gaps; a 0.5 mm coating on a liner changes the grinding chamber geometry. Thickness is therefore chosen per surface, and where a gap is critical the part is machined after spraying rather than coated to a nominal figure. On used mills, the worn profile is rebuilt first, otherwise the coating preserves a chamber that no longer classifies correctly.
Frequently asked questions
How long do coated crusher liners last?
In cathode material milling, three to five times the life of uncoated wear plate is typical, depending on the material hardness and the mill loading.
Can worn liners be recoated?
Yes, if the base plate is not deformed or cracked. The old coating is stripped, the plate is straightened and re-profiled, then recoated.
Does the coating slow down the milling process?
No. A smoother, harder liner surface reduces friction and can slightly improve throughput compared with a roughened worn plate.
Further reading: WC-Co vs Cr3C2-NiCr.