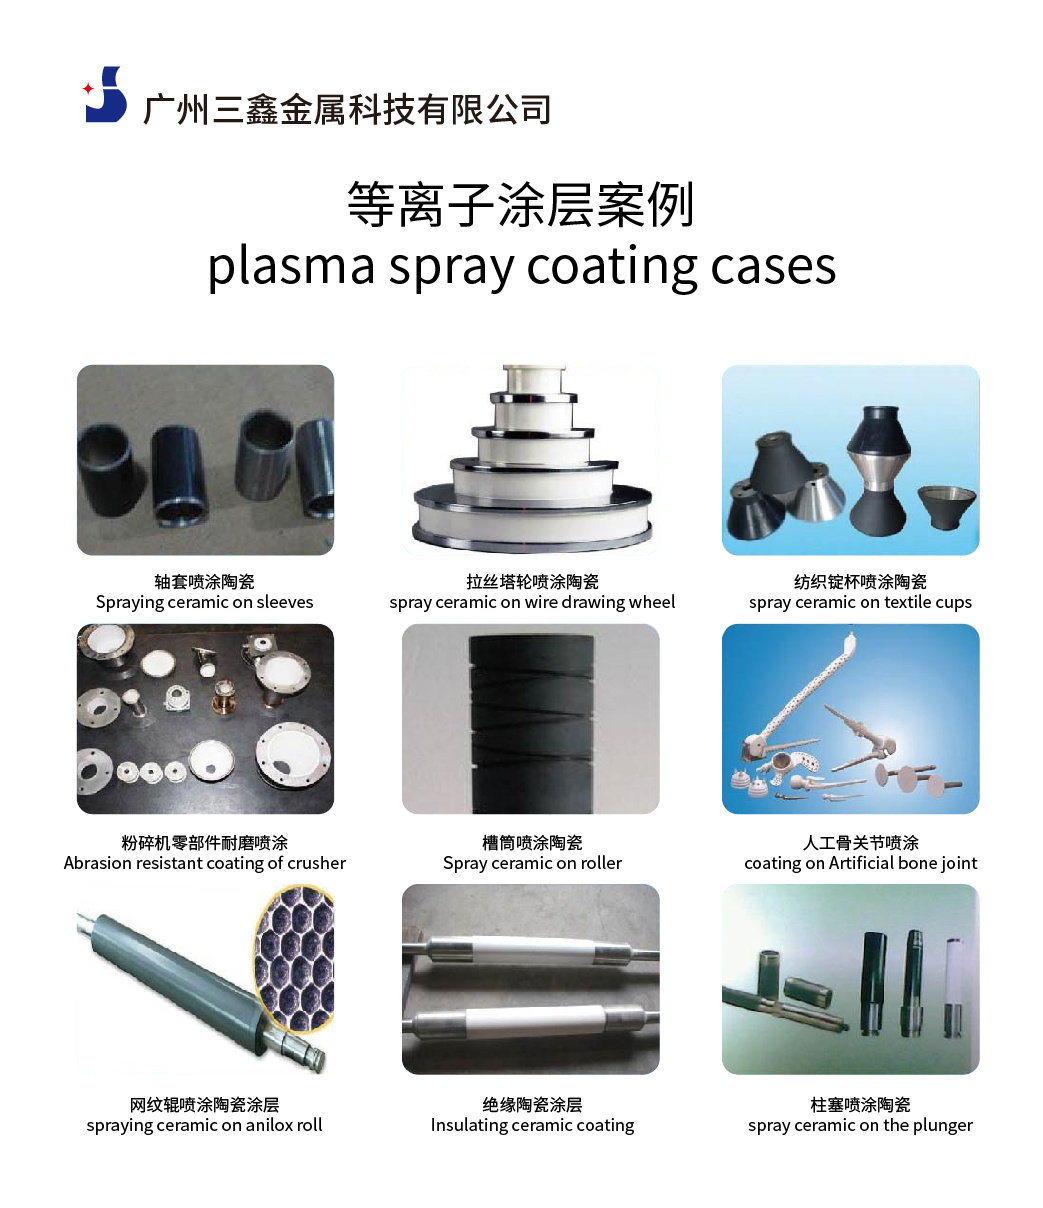
 Plasma spraying is a material surface strengthening and surface modification technology that uses a plasma arc driven by DC as a heat source to heat the ceramic material to a molten or semi-molten state, and spray it at high speed onto the surface of the pretreated workpiece to form a firmly adherent surface layer. Ceramic coatings prepared by plasma spraying have high bonding strength, low porosity and low surface roughness, and are increasingly used in repair and strengthening applications in various industries.
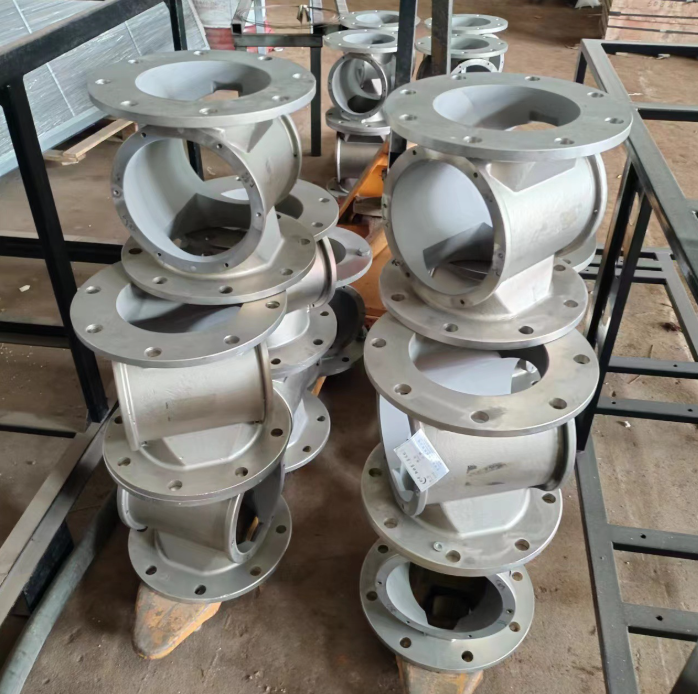
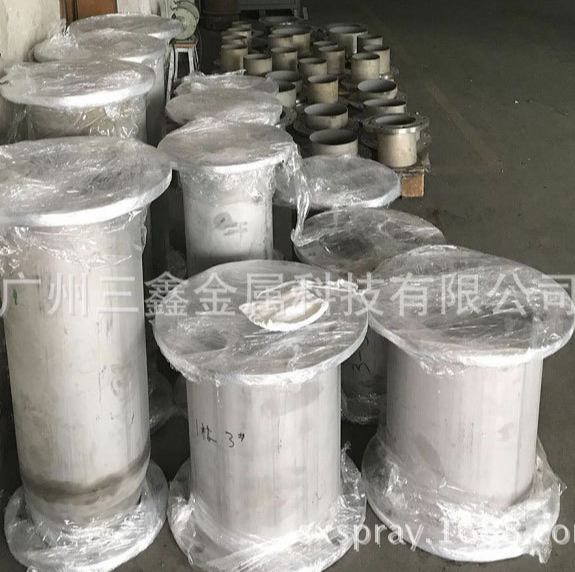
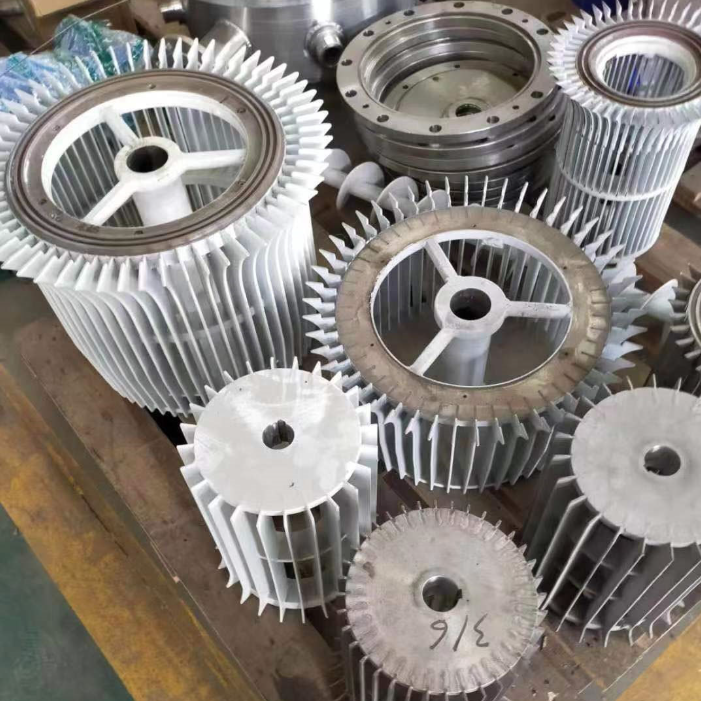
Process options
| Process | Typical thickness | Hardness | Best for |
|---|---|---|---|
| Plasma cladding (PTA) | 0.5-3.0 mm | HRC 55-65 with carbide addition | Severe wear, rebuildable parts, metallurgical bond |
| HVOF carbide | 0.10-0.40 mm | 1,050-1,300 HV0.3 | Sliding wear with impact, tight tolerance |
| Plasma ceramic | 0.15-0.50 mm | 900-1,100 HV0.3 | Acid and alkali resistance, insulation |
| Nano ceramic composite | 0.05-0.20 mm | Depends on system | Thin barrier coatings, sealing surfaces |
Cladding versus spraying - the real difference
Thermal spray produces a mechanical bond. Plasma cladding (PTA) melts a layer of the substrate and the additive together, producing a metallurgical bond with no porosity at the interface. That matters on parts that see heavy impact or thermal cycling, where a sprayed layer might spall. The cost is heat: the part reaches 800-1,000 °C locally, so distortion and post-weld heat treatment must be planned.
Choosing between them
If the part is thin, heat-treated, or dimensionally critical, spraying is the right route. If it is a heavy, low-value part that is being rebuilt repeatedly and sees impact, cladding is more durable and often cheaper over the life of the component.
Where this work is used
The same combination - strong acid or alkali, elevated temperature and abrasion - shows up in a predictable set of equipment: reactor and agitator internals in chemical plants, pickling line rolls and tanks in steel processing, slurry pump casings in fertiliser production, flue and scrubber components, and dies and screws in plastics and rubber processing. In each case the coating replaces a rubber or PTFE lining that fails at temperature, or a stainless grade that cannot carry the abrasion.
What the substrate has to be
Coating does not fix a substrate problem. The base metal must be sound, free of through-wall corrosion and able to take a blast profile; heavily pitted or graphitised cast iron is usually a no. Where the wall has been eaten thin, the repair starts with welding, and the coating goes on afterwards - which is why we assess wall thickness before quoting rather than after the part arrives.
Acceptance and documentation
For chemical plant work the record matters as much as the coating: thickness on a grid, hardness on a coupon sprayed in the same run, adhesion by pull test, and a holiday test where the coating is a barrier against the process liquid. Parts are photographed before and after, and the parameter set is filed so a repeat order reproduces the same result.
Frequently asked questions
Can a clad part be machined back to tolerance?
Yes. Cladding is applied oversize and finished by grinding or turning. Hardness above HRC 55 requires carbide tooling or grinding rather than turning.
Which handles strong acids better, ceramic or carbide?
Alumina and chromia are better in most acids; carbides are chosen where wear dominates and the acid is moderate. Where both are severe, a sealed ceramic over a corrosion-resistant bond coat is used.
How do I decide between repair and replacement?
As a rule, if the part costs more to replace than roughly 30% of its value and the substrate is sound, rebuilding is worth quoting.
Further reading: What drives coating cost per part.