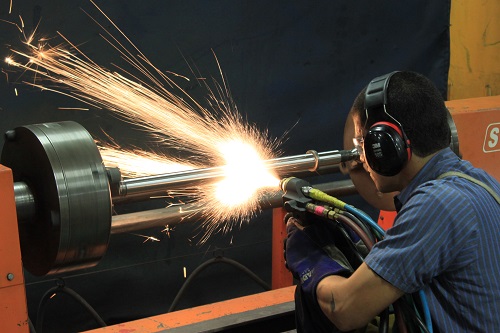
Buyers often expect thermal spray to be priced like painting - a rate per square metre, applied uniformly. It is not. The same drawing sent to three shops can come back at 300, 600 and 1,100 USD, and all three quotes can be honest. The difference lies in how much of the powder actually lands on the part, how much labour the geometry consumes, and how much grinding the tolerance demands.
Here is how the cost of a coated part is actually built up, and where the leverage is.
The cost structure
| Cost element | Share of total | What drives it |
|---|---|---|
| Powder material | 20-35% | Material type, coating volume, deposition efficiency |
| Spray time and labour | 25-35% | Area, spray rate, number of passes, handling |
| Preparation and masking | 10-15% | Geometry, number of masked features, degreasing and blasting time |
| Grinding and finishing | 10-20% | Tolerance, surface finish, hardness of the coating |
| Inspection and documentation | 4-8% | Thickness mapping, bond tests, hipot, reports |
| Setup and overhead | 10-15% | Batch size, fixturing, programming |
1. Powder: the number buyers underestimate
Powder price varies by more than an order of magnitude, and it is charged on what you feed the gun, not what ends up on the part.
| Material | Indicative powder price (USD/kg) | Typical deposition efficiency |
|---|---|---|
| Alumina (Al2O3) | 15-35 | 55-70% |
| Chromia (Cr2O3) | 40-65 | 45-60% |
| Zirconia / YSZ | 60-120 | 45-60% |
| WC-Co | 45-85 | 45-60% (HVOF) |
| WC-CoCr | 55-95 | 45-60% (HVOF) |
| Cr3C2-NiCr | 70-120 | 40-55% (HVOF) |
Deposition efficiency is the share of fed powder that bonds to the part. On an open flat plate a well-tuned gun reaches 65-70%; on a 300 mm diameter roller with a narrow spray spot and overspray past both ends, 45% is realistic. Half the powder you pay for is captured by the booth filter.
2. Geometry: the hidden multiplier
Coating area is only part of the story. A roller is the cheapest geometry in thermal spray: the gun traverses, the part rotates, masking is two bands at the ends. A valve body with eight masked bores, blind pockets and a sealing face can take longer to mask than to spray. In small-lot work, masking and fixturing frequently exceed the spray time itself.
3. Thickness and finish: where tolerance costs money
Every 0.1 mm of coating is powder, spray time and grinding time. Spraying 0.4 mm and grinding back to 0.2 mm doubles the material cost to save on set-up; spraying 0.15 mm on a part that needs 0.25 mm means a rework. The economic allowance is normally 0.05-0.10 mm above final thickness for grinding.
4. Worked example
A 1.2 m² steel roller, HVOF WC-CoCr, 0.30 mm final coating, ground to Ra 0.4:
- Coating volume: 1.2 m² × 0.0003 m = 0.00036 m³. At a deposited density of about 12,500 kg/m³, that is roughly 4.5 kg of coating.
- At 50% deposition efficiency, powder fed is about 9 kg. At 60 USD/kg, powder cost is about 540 USD.
- Spray rate around 4 kg/h means roughly 2.3 spray hours; with handling and set-up allow 3.5 labour hours at 80 USD/h, about 280 USD.
- Degrease, blast and mask: about 200 USD. Diamond grinding: about 300 USD. Inspection and report: about 120 USD.
- Total in the region of 1,450 USD, or roughly 1,200 USD per m² of coated surface.
The same roller in plasma alumina at 0.8 mm uses cheaper powder but a thicker layer and a slower grind; it often lands in a similar range per square metre. The mistake is comparing processes on powder price instead of cost per finished part.
5. Six ways to reduce the price without reducing quality
- Batch the parts. Set-up is spread across the order; ten identical parts can cost 30-40% less per part than one.
- Reduce masked features. A design change that removes a masked bore or an O-ring groove can cut preparation time more than any powder negotiation.
- Do not over-specify thickness. Specify the minimum that survives the duty, not the maximum the drawing allows.
- Match the finish to the function. Ra 0.8 instead of Ra 0.2 can halve grinding time on a part that does not need a mirror surface.
- Use alumina where the duty allows. Zirconia and chromia cost two to four times more per kilogram for properties many applications never use.
- Supply clean, dimensionally consistent parts. Oversized or contaminated substrates add blasting and grinding time that shows up in the quote.
Frequently asked questions
Is there a standard price per square metre?
No, and any shop quoting one without seeing the drawing is guessing. Geometry, masking, thickness and finish move the number by a factor of two to three on the same material.
Why is my second order more expensive than the first?
Usually batch size or thickness change rather than a price increase. A single part carries the full set-up cost, and a thicker coating multiplies powder and grinding time.
Does a thicker coating last proportionally longer?
Not always. HVOF carbide beyond 0.4-0.5 mm accumulates residual stress and can spall; ceramic beyond 2 mm cracks. The optimum is a design window, not "as thick as possible".
What is the typical lead time?
Five to ten working days for standard steel parts in small batches, longer for oversized rollers, carbide finishing or when witness-coupon testing is specified. Rush handling is possible and is priced separately.