Application fields:
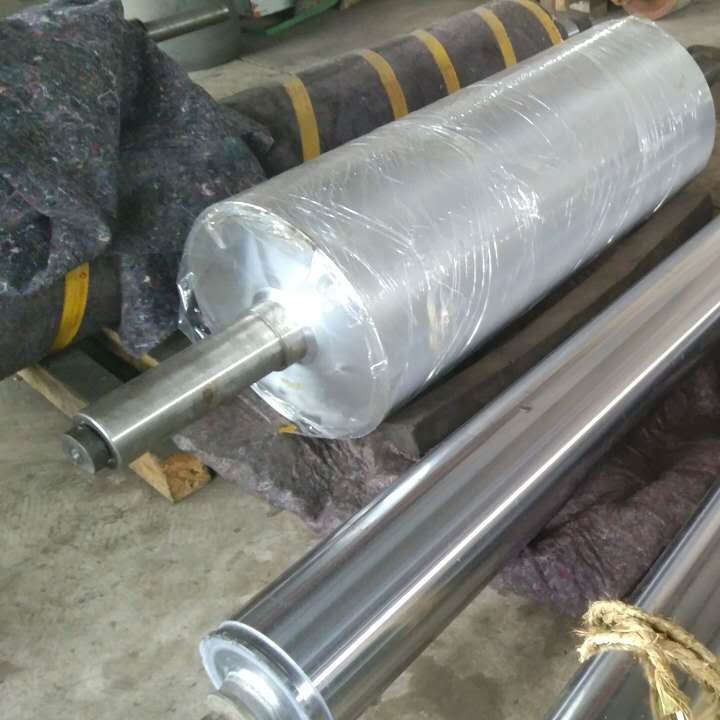
Centrifugal and screw pump shafts, hydraulic and pneumatic piston rods, plungers in reciprocating pumps and compressors, valve stems, and similar seal-carrying surfaces.
Technical principles and processes:
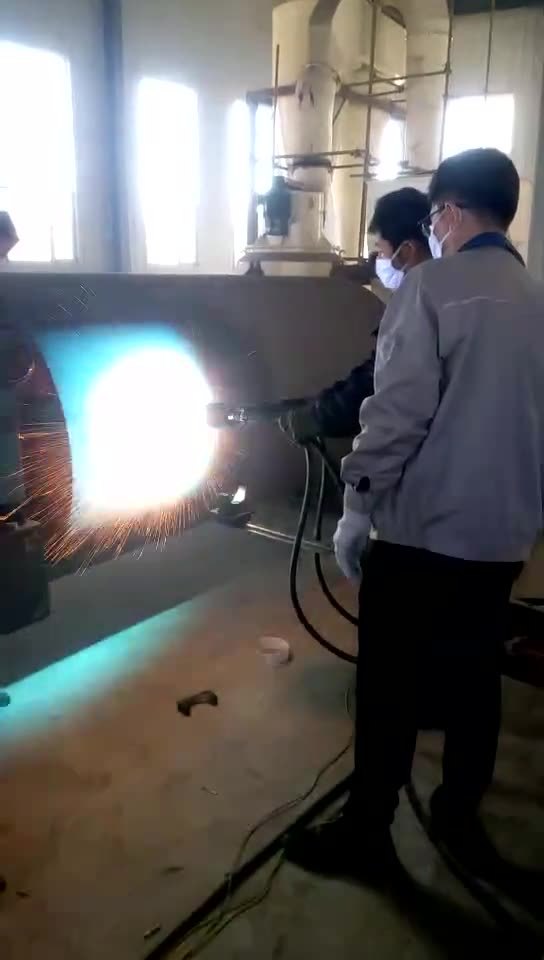
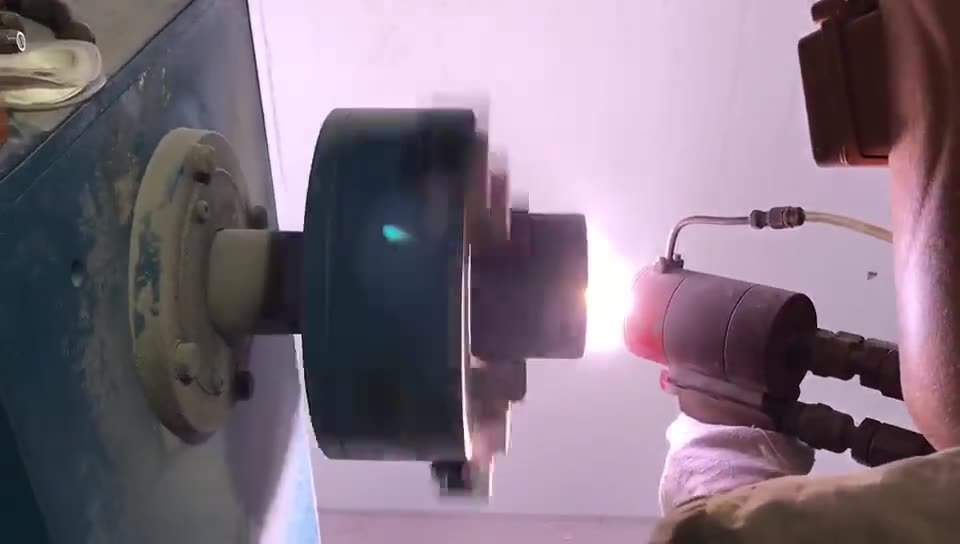
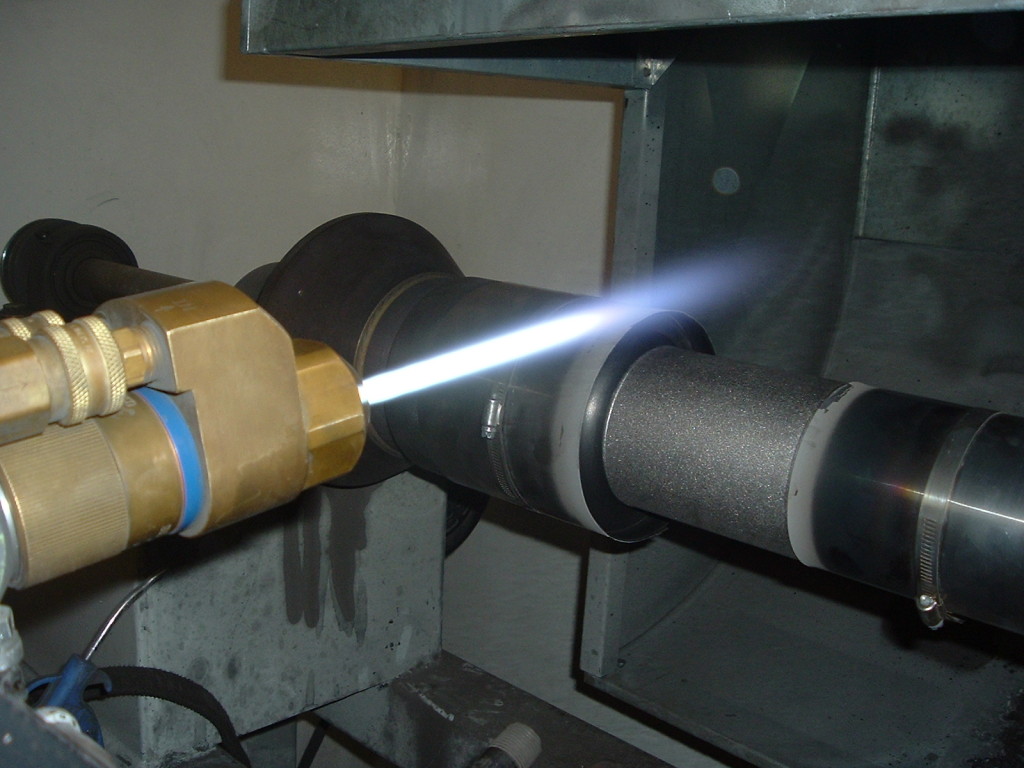
The shaft is degreased, masked at the seal and bearing seats, and grit blasted. A tungsten carbide-cobalt or carbide-nickel-chrome powder is sprayed by HVOF to form a dense coating, which is then finish ground and polished to the required diameter, roundness and Ra, so the seal runs on a smooth hard surface.
Coating performance:
- Micro-hardness 1100-1400 HV with very low porosity
- Coating thickness 0.10-0.30 mm, ground to final diameter
- Surface finish to Ra 0.2 for seal and packing contact
- Resistant to wear, fretting and many corrosive media
- Roundness and straightness verified after grinding
泵轴与活塞杆 HVOF 碳化钨涂层:针对密封配合面磨损导致泄漏的问题,用超音速火焰喷涂碳化钨并磨削抛光,获得致密、高硬、耐蚀的密封工作面。
Coating specification
| Parameter | Typical value |
|---|---|
| Coating | WC-10Co-4Cr (corrosion grade) or WC-12Co (impact grade) |
| Thickness | 0.10-0.30 mm, ground after spraying |
| Microhardness | 1,050-1,300 HV0.3 |
| Porosity | Below 1% |
| Bond strength | 70 MPa minimum (ASTM C633) |
| Surface finish | Ra 0.2-0.4 in the seal zone; Ra 0.1 available |
| Diameter tolerance | ±0.01 mm, cylindricity 0.005 mm |
| Maximum service temperature | 450 °C continuous |
Why HVOF and not hard chrome
Hard chrome plating is the traditional answer for pump shafts, and it works - until it doesn't. Chrome is brittle, it cracks in a network that reaches the substrate, and those cracks become corrosion paths in chloride service. HVOF tungsten carbide is applied at low substrate temperature, has less than 1% porosity, and the cobalt-chromium matrix tolerates chlorides far better. In seawater pumps it commonly outlasts chrome by three to five times.
What we need to quote a shaft
- Drawing with the finished diameter and the tolerance on the seal zone.
- Current condition: new part, worn, or previously chrome plated (chrome must be stripped first).
- Pump medium, temperature, and whether solids are present.
- Straightness limit - long shafts may need support during spraying and straightening afterwards.
Why the seal surface is the whole job
A pump shaft does not fail because the shaft is weak - it fails because the running surface under the seal or packing wears, the gap opens, and the pump starts to leak. That is why the coating specification is written around the seal interface: thickness, finish and roundness there matter far more than the coating on the rest of the shaft.
Finish and roundness requirements
| Seal type | Typical finish | Note |
|---|---|---|
| Mechanical seal (O-ring) | Ra 0.2-0.4 um | Ground and polished; no spiral marks |
| Gland packing | Ra 0.4-0.8 um | Slightly rougher holds lubricant film |
| Labyrinth / clearance bush | Ra 0.8-1.6 um | Roundness dominates over finish |
Corrosion under the seal
Piston rods and pump shafts often corrode in the stagnant zone just outside the seal, where the process liquid sits and evaporates. A dense HVOF carbide layer with sealed porosity resists that attack; an unsealed or thin coating pits there first, and the pitting then acts as a stress raiser under the seal. That is why we specify the coating to extend past the seal travel, not just under it.
Reconditioning a worn shaft
A shaft that has worn below the seal tolerance is not simply coated: the worn area is measured, any corrosion pits or scores are removed by grinding, and the section is built back to slightly above nominal before the carbide is applied. Grinding back to the drawing dimension then leaves a coating of uniform thickness rather than a patch over a damaged surface.
Frequently asked questions
Can a worn shaft be built back to size?
Yes, up to about 0.5 mm of diametral build-up with carbide. Beyond that an arc sprayed build-up layer is applied first, then finished with HVOF carbide.
Does the coating need sealing?
Not for wear. For chloride or acid service a sealer is applied to close the residual porosity and extend corrosion life.
Will the shaft need rebalancing?
Normally not - the coating is symmetrical. High-speed shafts are checked for runout after grinding.
Further reading: WC-Co vs Cr3C2-NiCr.
Further reading: replacing hard chrome with HVOF carbide.