One Workshop, All Thermal Spray Processes
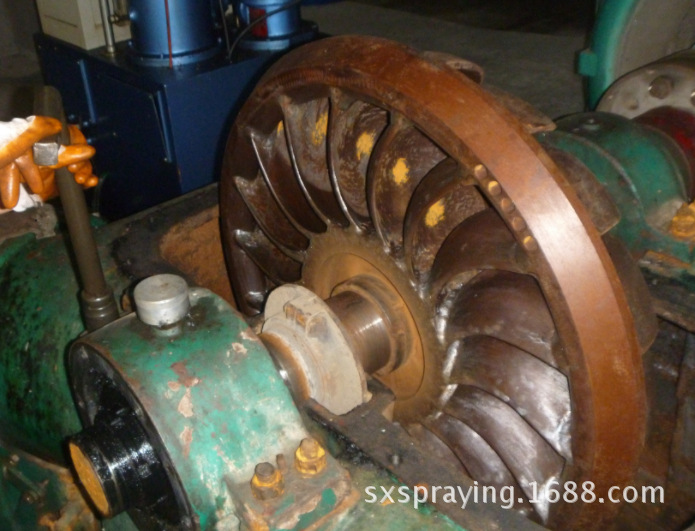
We operate plasma, HVOF, arc and flame spraying under one roof, so the process is chosen to fit the part and the duty instead of the other way round. Ceramic, carbide, metallic and self-fluxing alloy powders and wires are all in routine production.
Coating Families
- Ceramic coatings (Al2O3, Cr2O3, ZrO2, AT): wear, insulation, high temperature.
- Carbide coatings (WC/Co, Cr3C2/NiCr by HVOF): extreme sliding and particle erosion resistance.
- Metal and alloy coatings (Zn, Al, NiCr, stainless by arc spray): large-area anti-corrosion and build-up.
- Non-stick and release coatings for cookware, moulds and rolls.
Industries Served
Machinery manufacturing, energy and power, mining and metallurgy, petrochemical, paper and printing, packaging, aviation and general machinery maintenance.
How We Work
- Send the drawing or a photo of the part together with the working condition.
- We propose the coating system, process parameters and finishing method.
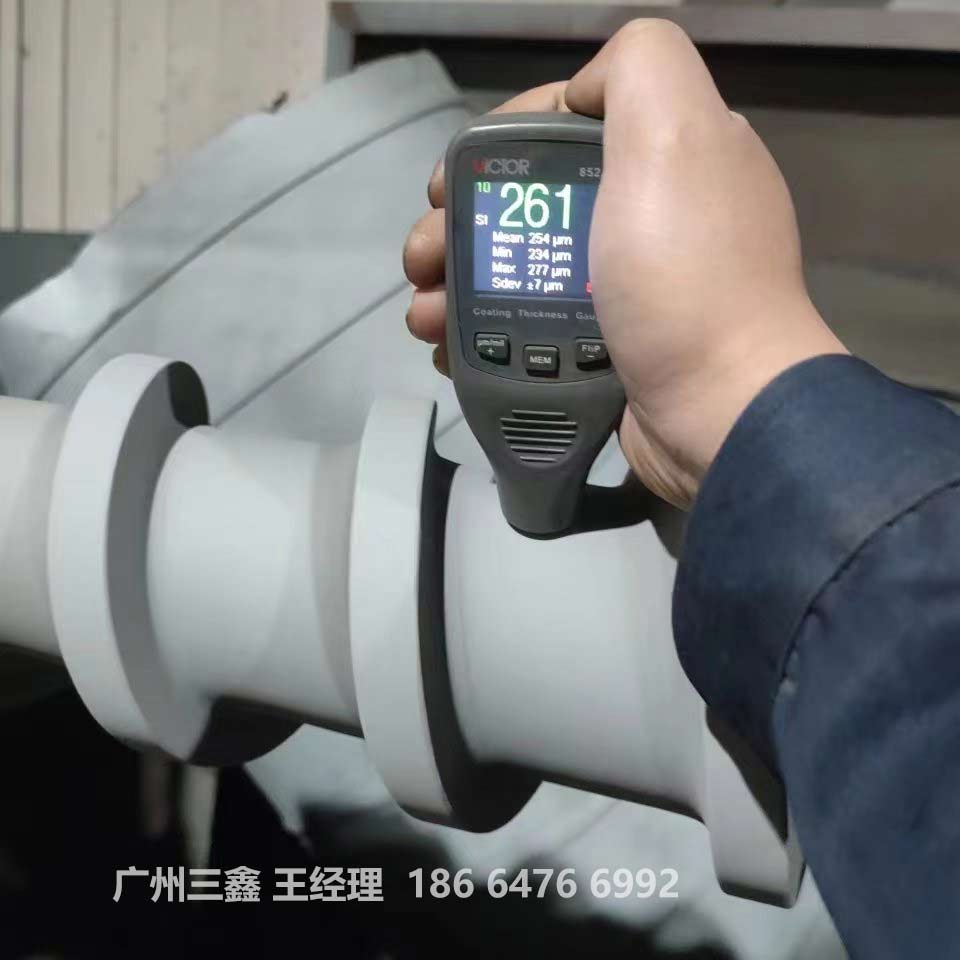
- Parts are sprayed, sealed, finish-ground or polished, and inspected for thickness, bond and roughness before delivery.
- Equipment supply, on-site spraying and process training are available in addition to workshop coating.
Process selection guide
We run four processes in one shop, so the recommendation is based on the duty rather than on what a single gun happens to do well.
| Process | Coating material | Thickness | Best for |
|---|---|---|---|
| HVOF | WC-Co, WC-CoCr, Cr3C2-NiCr | 0.05-0.5 mm | Sliding abrasion, erosion, hydraulic rods, pump shafts |
| Plasma (APS) | Al2O3, Cr2O3, ZrO2, TiO2 | 0.10-2.0 mm | Insulation, dielectric layers, thermal barrier, chemical resistance |
| Arc spray | Zn, Al, Zn-Al, Ni-Al, stainless | 0.10-3.0 mm | Large-area anti-corrosion, dimensional build-up |
| Flame spray | Ni-based self-fluxing alloys | 0.20-1.5 mm | Repair of worn shafts and seals, fusible coatings |
What is included in every order
- Drawing and duty review before quoting - we confirm the failure mode, not just the coating name.
- Degreasing, grit blasting and masking, with blasted surfaces sprayed the same shift.
- Witness coupon sprayed with the batch for bond strength and porosity testing.
- Grinding or polishing to drawing tolerance, with thickness mapping at defined points.
- Inspection report: thickness, microhardness, roughness, bond strength, and dielectric test where applicable.
Typical lead time
Five to ten working days for standard steel parts in small batches; two to three weeks for oversized rollers with finish grinding, or when a full metallurgical report is specified.
Frequently asked questions
Can you coat parts we have already machined to final size?
Yes, but leave a grinding allowance. We normally require 0.05-0.10 mm above final coating thickness so the surface can be ground after spraying. Sending a part already at final size usually means the coating has to be thinner than the duty requires.
Do you coat one-off parts?
Yes. Single parts are routine; they simply carry the full set-up cost, which is why per-part price falls sharply with batch size.
What information do you need for a quote?
A drawing with tolerances, the substrate material, the working temperature, the counter-material or medium causing wear, and any electrical or chemical requirement. That is enough to recommend a process and price it.
Further reading: HVOF vs plasma spraying and what drives coating cost per part.