Application fields:
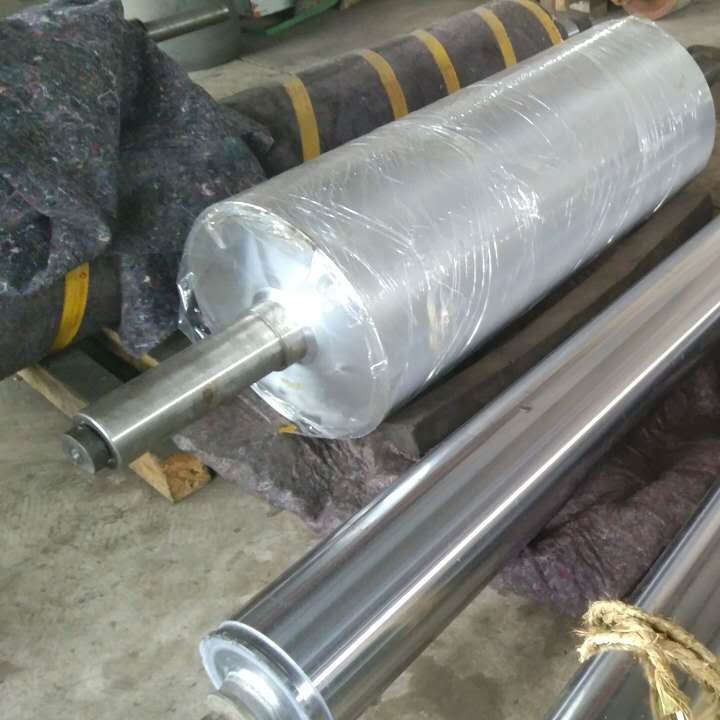
Crane and trolley wheels, sheave wheels and rope drums, large fan and pump discs, brake discs and drums, mill and kiln tyres, and other heavy rotating parts.
Technical principles and processes:
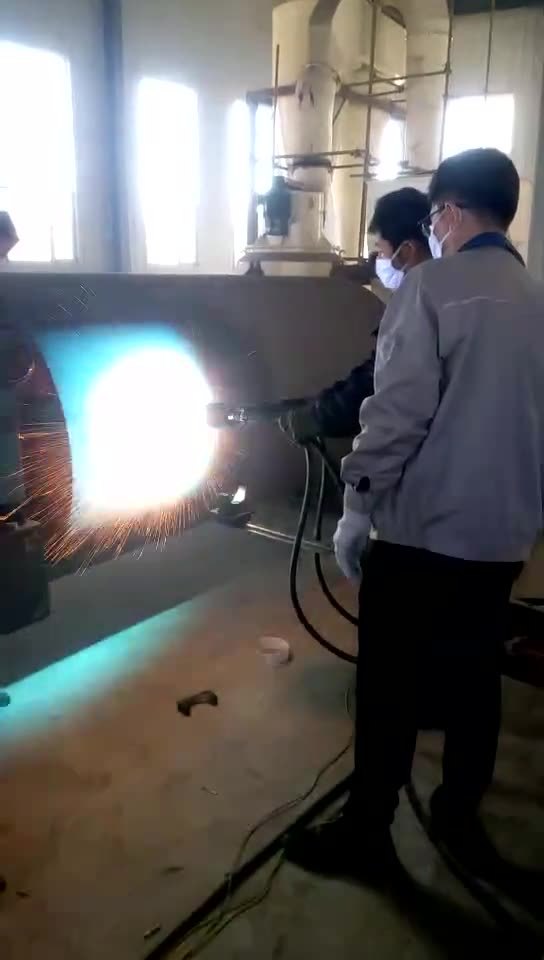
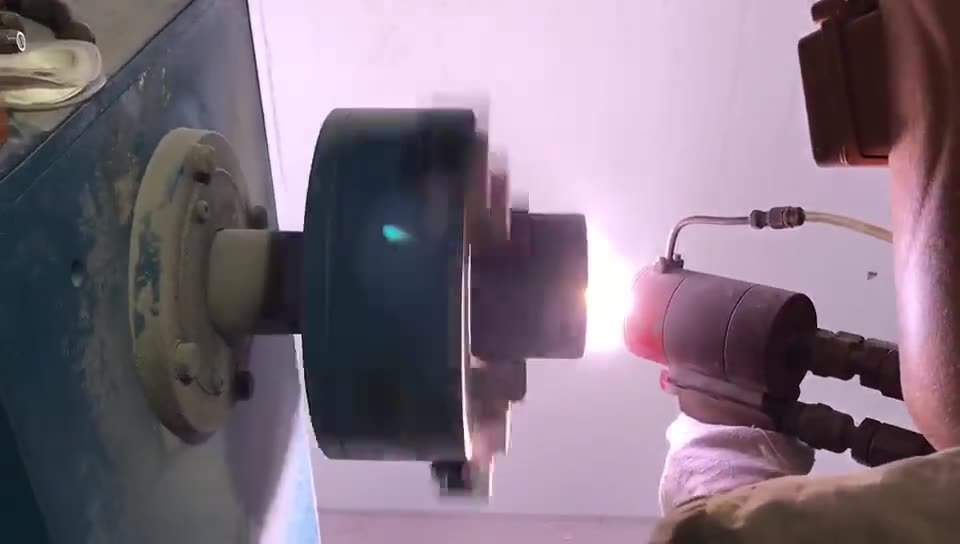
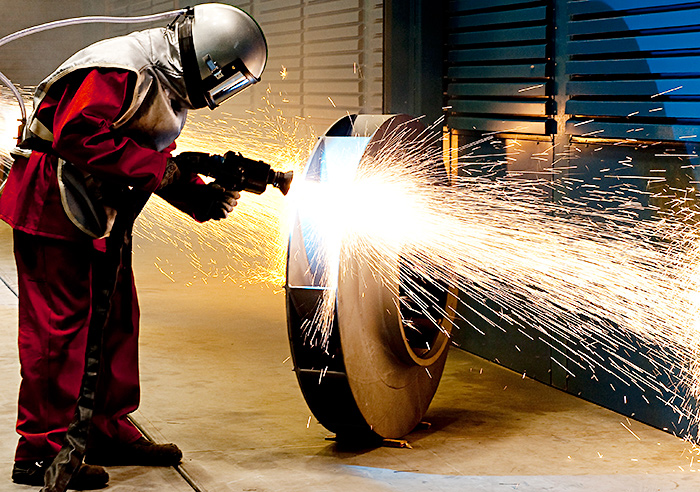
The part is cleaned, grit blasted and, where wear is significant, pre-machined to accept the coating. Metal wire is arc sprayed to build up the surface or to apply a protective layer, and the part is then machined or ground back to the required diameter and profile.
Coating performance:
- Deposit rates high enough for large components and deep build-up
- Rebuilds surfaces worn by several millimetres
- Wire options include carbon steel, stainless steel, bronze and zinc alloys
- Machined and ground to drawing diameter and profile
- Lower cost and shorter lead time than new part replacement
大型轮盘与回转件电弧喷涂:针对天车轮、绳轮、卷筒、风机盘等大型件,用电弧喷涂恢复尺寸并附加耐磨或防腐层,成本远低于换新。
Coating options
| Wire | Coating | Typical use |
|---|---|---|
| Carbon steel | Build-up and dimensional restoration, 0.5-3.0 mm | Crane wheels, sheaves, mill tyres |
| Bronze | Low friction, good bearing behaviour | Rope drums, sliding surfaces |
| Stainless (420 / 316) | Wear plus corrosion resistance | Wheels in wet or chemical environments |
| Zn-Al 85/15 | Sacrificial corrosion protection | Structural discs exposed outdoors |
Why arc spray suits large rotating parts
Arc spray has the highest deposition rate of any thermal spray process - 10-30 kg/h - and the equipment is portable. On a 1.5 m crane wheel with a worn flange, that means the part can be built back in hours rather than replaced, and often without dismantling the crane. Coating thickness up to 3 mm is practical, which is far beyond HVOF or plasma.
The trade-off is porosity, typically 3-8%, and lower bond strength than HVOF. For dimensional restoration that is acceptable - the coating is a build-up layer, not a wear surface, and it is usually machined back to the original profile.
Why arc spray for large rotating parts
On a wheel or disc of a metre or more, the coating area is the cost driver, and arc spraying deposits metal several times faster than plasma or HVOF. For anti-corrosion or dimensional restoration with a metallic layer, that speed is the difference between an economical repair and a replacement part - and the process runs at a standoff that suits a large rotating workpiece.
Balance and runout
Coating a large rotating part means adding mass. The layer is applied evenly around the circumference, the part is machined after spraying, and balance is checked before it goes back into service. Runout on the coated face is measured as well, because an uneven layer on a fast wheel shows up as vibration long before it shows up as wear.
Where arc spray is the wrong process
Arc spray deposits wire metal, so it cannot produce a carbide or ceramic wear layer. Where the duty is abrasive rather than corrosive, plasma or HVOF with carbide powder is the correct choice, even at higher cost per square metre. We specify by duty, not by which process is cheapest to run.
Coating versus hard-facing
For a very large wheel that has lost several millimetres, arc spray can rebuild the section, but hard-facing by welding may be the better choice where impact is severe. Arc sprayed metal is mechanically bonded and relatively porous; a weld overlay is metallurgical and tougher, at the cost of heat input and distortion. The size and heat sensitivity of the part usually decide.
Frequently asked questions
How thick can arc spray build up?
Up to 3 mm in a single setup for steel wire. Thicker builds are possible in layers, but residual stress rises and edge chipping becomes the limiting factor.
Can it be done on site without removing the wheel?
Often yes. Our portable arc spray units have been used on crane wheels, rails and sheaves in place, with local extraction and masking.
Does the repaired wheel need to be re-machined?
Yes for most running surfaces. The coating is sprayed oversize and turned or ground back to the original profile and hardness requirement.
Further reading: HVOF vs plasma spraying.